High-precision diamond cutting discs engineered for zero-chipping performance across dense porcelain, sintered stone, and hard granite matrices.
A Deep Technical Analysis into Sintering Metallurgy, Synthetic Diamond Micro-Grit Distribution, and Thermal Dissipation Mechanics for Ultra-Hard Materials.
Modern ceramic materials, particularly sintered stone (such as Dekton, Neolith, and Lapitec), exhibit extreme Mohs hardness (7.5–8) coupled with high internal tension. Cutting these materials without macro-chipping or thermal fracturing requires a meticulously engineered metallurgical bond. At JIAYAN Superhard Materials Co., Ltd., our manufacturing process utilizes cold-pressing followed by vacuum hot-pressing sintering technology. This bonds synthetic diamond crystals (MBD/SBD series) inside a custom cobalt-nickel-copper-bronze alloy matrix.
The matrix retention strength is dynamically calibrated to match the friability of synthetic diamonds. As diamond edges dull under friction, the surrounding metal matrix wears away at a controlled rate—exposing fresh, sharp diamond micro-points (self-sharpening mechanism). This minimizes lateral vibration, reduces blade deflection, and ensures smooth, mirror-finish cuts on vitreous ceramic surfaces.
When operating at circumferential speeds exceeding 35 m/s, thermal expansion differences between the high-carbon 75Cr1 steel core and the sintered diamond segments can induce warp and radial run-out. To mitigate structural distortion, our premium ceramic blades incorporate precision laser-cut J-slots and keyhole gullets.
These engineered expansion slots serve a dual purpose: first, they act as mechanical stress-relief zones that absorb thermal expansion; second, they form optimized hydrodynamic channels that force coolant deep into the kerf. This rapidly flushes out dense ceramic slurry, preventing segment clogging (loading) and significantly reducing friction-induced heat generation during continuous industrial bridge-saw operations.
Rigorous engineering benchmarks across our full spectrum of diamond circular saw blades and ceramic cutting discs.
| Blade Outer Diameter | Segment Specs (L x W x H) | Bore / Arbor Sizes | Target Substrate / Material | Recommended RPM | Cooling Mode |
|---|---|---|---|---|---|
| 105mm – 125mm (4"–5") | Continuous Rim / Mesh 1.0–1.2mm | 20mm / 22.23mm / M14 | Ceramic Wall/Floor Tiles, Ultra-Thin Porcelain | 11,000 – 13,300 RPM | Dry / Wet Dual Use |
| 250mm – 300mm (10"–12") | J-Slot Segment / 2.0–2.4mm | 25.4mm / 50mm / 60mm | Sintered Stone, Porcelain Slabs, Marble | 2,800 – 3,600 RPM | Wet Cutting Required |
| 350mm (14") Specialized | 3.0mm Segment / 10mm–15mm Height | 50mm / 60mm High Precision | Dense Granite, Hard Sintered Slabs, Quartzite | 1,800 – 2,450 RPM | High-Pressure Wet Cooling |
| 400mm – 600mm Industrial | 3.6mm–4.2mm Silent Core Segments | 60mm / Custom Flange | Granite Blocks, Heavy Engineered Stone | 1,200 – 1,600 RPM | Continuous Wet Operation |
Tailored blade formulations optimized for specific regional material characteristics, fabrication habits, and machinery standards.
In markets like Italy, Spain, and Germany, 12mm to 20mm ultra-compact sintered porcelain slabs (e.g., Dekton, Neolith) dominate luxury architectural design. Fabricators require absolute edge precision for 45-degree miter joints without edge chipping. JIAYAN's 14" J-Slot Continuous Rim blades utilize fine micro-grit diamonds (170/200 mesh) to achieve clean cut faces ready for seamless epoxy assembly.
North American stone shops routinely process abrasive Class 4 and 5 natural granites alongside hard engineered quartz. Our 350mm OEM granite blades feature high diamond concentration (28% by volume) with a cobalt-reinforced bond, ensuring fast feed rates (up to 3.5 meters/min) on CNC bridge saws while retaining exceptional tool lifespan.
Across Southeast Asia, the Middle East, and Latin America, high-volume residential construction demands fast, dry-cutting hand-angle grinder blades. JIAYAN's 1.0mm ultra-thin mesh turbo blades reduce friction resistance, lower power load on cordless tools, and prevent burning during rapid ceramic wall tile trimming.
Leveraging complete industrial clusters, raw material integration, and fully automated sintering lines to deliver unbeatable procurement value.
Located in Wuhu, China, and operating within the heart of the national superhard material ecosystem, JIAYAN Superhard Tools benefits from direct proximity to synthetic diamond synthesis hubs and high-purity metal powder refineries. As an active member of the China Superhard Material Association, our supply chain bypasses intermediaries, allowing us to secure top-tier raw synthetic diamond crystals (high-TI/TTI single crystals) at optimized cost levels.
This integration translates directly into commercial advantages for global distributors: robust pricing stability, guaranteed diamond concentration consistency, and rapid production scale-up capacity—even during global raw material price fluctuations.
Our production facilities utilize automated multi-stage hot-pressing sintering presses, laser-welding robotic cells, and 100% automated segment alignment machines. Every batch of diamond saw blades undergoes rigorous quality verification:
Pioneering the future of superhard abrasive engineering through advanced materials science and smart manufacturing.
Implementation of Ti/Cr chemical vapor deposition (CVD) coatings on synthetic diamond grains. The nanometer titanium layer acts as a thermal barrier and mechanical anchor, increasing diamond retention strength within the metal bond by up to 35% and extending tool life significantly.
Development of multi-layer sandwich steel cores utilizing viscoelastic copper foil laminates between hardened steel plates. Designed for urban indoor installation sites, reducing operational noise emissions by over 12 dB(A) while preserving high rigidity.
Transitioning toward environmentally compliant, cobalt-free sintered matrices based on iron-copper-tin advanced powder alloys. Lowering environmental impact while maintaining structural hardness and wear resistance equivalent to cobalt-rich formulations.
Demonstrating technical leadership and persistent engagement across international ceramic and stone machinery expos.
Our research team publishes technical standards covering non-destructive testing, microstructure analysis, and shear torque evaluation for high-safety laser-welded diamond blades used in heavy construction.

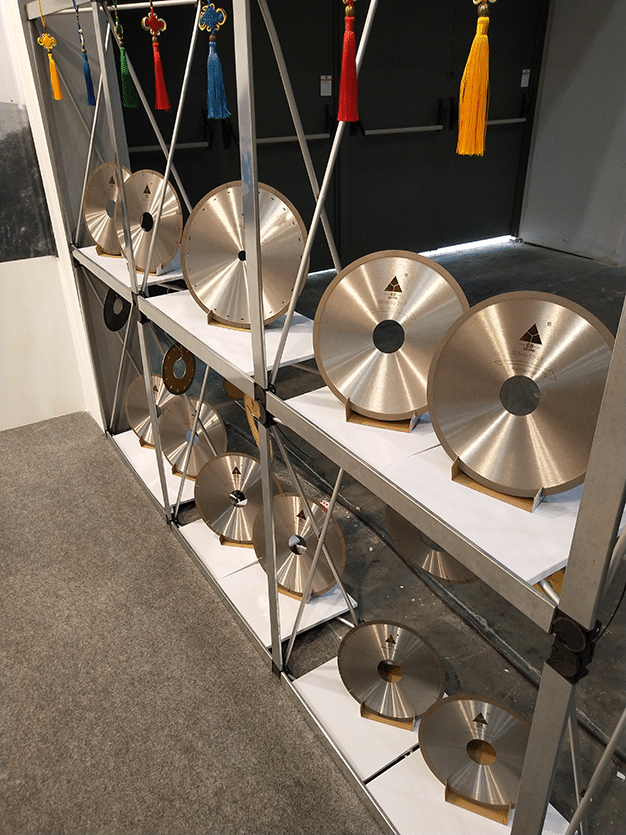
JIAYAN showcased specialized ceramic continuous rim blades and fast-cutting J-slot series at the Canton Fair Complex, establishing OEM partnerships with major machinery manufacturers across Southeast Asia and Europe.

Presenting next-generation sintered stone blades to European stone machinery integrators at Italy's flagship ceramic industry event, confirming JIAYAN's alignment with global precision cutting requirements.
Expert technical responses to common questions raised by industrial buyers, tool distributors, and plant managers.
Edge chipping is caused by excessive vibration, improper diamond grit size, or a matrix bond that is too hard, which leads to blade glazing. JIAYAN's specialized sintered stone blades utilize fine-mesh diamond grits embedded in a self-sharpening cobalt-bronze matrix combined with laser-cut J-slots. This design minimizes radial deflection, dampens micro-vibrations, and maintains a continuous sharp diamond edge for chip-free results.
Small-diameter discs (105mm to 125mm) with continuous rim or mesh turbo designs are engineered for both dry and wet cutting on hand-held angle grinders. However, for large-diameter blades (250mm to 350mm+) used on bridge saws or table saws, wet cutting with continuous water coolant is strictly required to prevent matrix overheating, steel core warping, and premature diamond degradation.
We offer comprehensive OEM/ODM customization including core arbor hole reaming (20mm, 22.23mm, 25.4mm, 50mm, 60mm with custom pinholes), custom segment height (up to 15mm), specialized diamond concentration levels, laser-engraved customer logos, customized color coating, and branded retail packaging.
For standard catalog products, our MOQ starts at 50 pieces per size. Custom OEM orders typically require an MOQ of 100 to 200 pieces depending on blade diameter. Production lead time is generally 15 to 25 calendar days from sample confirmation, supported by expedited air freight or sea freight shipping from major Chinese ports.
Direct factory export ordering across our full spectrum of superhard stone and ceramic cutting discs.










