Engineered with multi-stage hot pressing technology, optimized bond matrices, and synthetic diamond grains for maximum blade life and zero-chipping performance.

Diameter: 105mm - 350mm
Sintering: Hot-Press Sintered
Application: Porcelain, Tile, Marble
Kerf Thickness: 1.2mm - 2.2mm

Diameter: 14" (350mm / 260mm)
Sintering: Hot Pressed Matrix
Application: Dekton, Neolith, Slabs
Core Steel: Silent Sandwich Core

Diameter: 350mm (14 Inch)
Segment Height: 10mm / 12mm / 15mm
Application: Hard Granite, Quartzite
Bond Hardness: Medium-Hard Alloy

Diameter: 350mm
Sintering: High Temp Hot Press
Application: Granite, Engineered Stone
Speed Rating: 80 m/s Peripheral

Diameter Range: 4" to 5" (105-125mm)
Arbor Bore: 20mm / 22.23mm
Application: Angle Grinder Cutting
Usage: Dry & Wet Dual Purpose

Diameter: 350mm (14 Inch)
Rim Type: Smooth Continuous
Application: Glazed Ceramic, Vitrified
Edge Finish: Chip-Free Precision Cut

Diameter: 350mm
Segment Design: Keyhole Slot Segmented
Application: Industrial Ceramic & Stone
Cooling: Rapid Heat Dissipation

Kerf Thickness: 1.0mm / 1.2mm Ultra-Thin
Core Reinforcement: Flange Reinforced
Application: Precise Porcelain Edging
Feature: Low Material Loss Rate
An authoritative analysis of powder metallurgy, thermal compaction kinetics, and phase transformations in superhard tool manufacturing.
In modern superhard material manufacturing, Hot Press Sintering (HPS) represents the pinnacle of powder metallurgy for diamond cutting tools. Unlike cold pressing (which compacts powder at room temperature prior to pressureless sintering), hot pressing applies high uniaxial hydraulic pressure (typically 15 to 35 MPa) simultaneously with elevated temperatures ranging from 750°C to 980°C within high-purity graphite molds.
This concurrent application of thermal and mechanical energy fundamentally alters the densification mechanics. Thermally activated solid-state diffusion and localized liquid-phase formation occur rapidly, eliminating internal porosity and forcing the metallic alloy matrix (composed of Cobalt, Bronze, Iron, Nickel, and Tungsten Carbide) to achieve over 99.2% of theoretical density.
For global procurement teams, stone fabricators, and OEM distributors, hot-pressed diamond blades deliver exceptional mechanical lock on synthetic diamond grains (such as MBD-8 and MBD-12 grades), preventing premature diamond pull-out during heavy feed-rate cutting of ultra-dense substrates like granite, quartz, and sintered porcelain slabs.
By adjusting Cobalt-Iron-Copper ratios, JIAYAN engineers calibrate matrix hardness from HRB 75 (for extra hard quartzites) to HRB 105 (for highly abrasive sandstone), keeping diamond sharpness optimized.
Micro-fragmenting synthetic diamond crystals continuously expose fresh micro-cutting edges under impact, maximizing cutting speed while maintaining smooth surface edge finishes.
Saw blade steel cores (65Mn / 75Cr1) undergo tension leveling and laser balancing, preventing axial runout, vibration noise, and blade warping during high RPM operation.
Member of the China Superhard Material Association. Over a decade of direct export experience serving stone fabricators, construction contractors, and tool distributors worldwide.

Located in Wuhu, Anhui Province, China, JIAYAN Superhard Materials Co., Ltd. operates an advanced 15,000 m² manufacturing plant equipped with automated multi-station hot-pressing sintering presses, laser segment welding units, automatic segment grinding cells, and dynamic balancing testers.
As a verified member of the China Superhard Material Association, our factory adheres to ISO9001:2015 quality management protocols and EN13236 European safety requirements for diamond abrasive tools. Every batch of hot-pressed saw blades undergoes strict shear strength testing, runout inspection (less than 0.05mm), and high-speed destruction testing prior to global shipment.

Automated atmosphere-controlled hot sintering furnaces ensuring precise thermal soak cycles and uniform density.

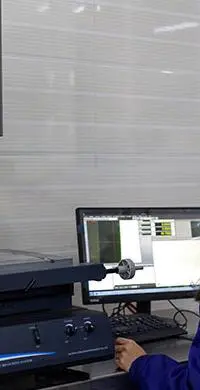
Optical profile inspection, tension analysis, and 100% shear stress testing on every production lot.
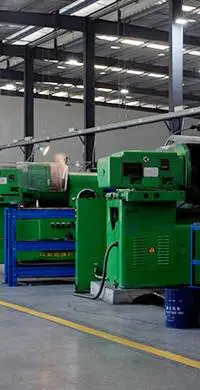
Monthly output of over 250,000 diamond saw blades and cutting discs for rapid containerized shipment.
Custom laser branding, blade color coating, segment engineering, and tailored retail packaging.
Tailored blade geometries, slot designs, and matrix formulations optimized for specific industrial stonework and masonry environments.
Sintered stone slabs present extreme hardness paired with internal stress tension, making them prone to edge chipping or slab cracking during bridge saw cutting. JIAYAN's specialized J-Slot Hot-Pressed Diamond Saw Blades combine a soft, self-sharpening cobalt-bronze matrix with narrow radial J-slots that dissipate heat instantly, maintaining pristine 90-degree edge finishes without micro-fracturing delicate surfaces.
Processing Class IV and Class V hard granites (e.g., Black Galaxy, Kashmir White) requires aggressive diamond exposure and high impact resistance. Our 350mm hot-pressed segmented circular blades utilize high-concentration synthetic diamonds (40/50 mesh) bound in a tough tungsten-iron matrix, enabling cutting speeds up to 1,500 mm/min on heavy bridge saws.
For interior tile installers and commercial flooring contractors, our 1.0mm to 1.2mm ultra-thin continuous rim blades provide swift dry and wet cutting. The continuous hot-pressed rim prevents material waste, while reinforced center flanges eliminate flex during freehand angle grinder operations.
In municipal infrastructure and building demolition, hot-pressed turbo blades feature aggressive wave segments that eject abrasive concrete slurry rapidly while protecting the steel core against undercut wear, extending operational life by 35% compared to standard cold-pressed discs.
Maximize blade life and cutting efficiency by matching peripheral linear velocity (m/s) and water flow rate to material hardness.
| Material Category | Blade Diameter (mm / inch) | Optimal RPM Range | Peripheral Speed (m/s) | Coolant Flow (L/min) | Recommended Rim Profile |
|---|---|---|---|---|---|
| Sintered Stone / Dekton | 350mm / 14" | 1,800 – 2,200 RPM | 30 – 38 m/s | 15 – 20 L/min (Wet Only) | J-Slot / Continuous Rim |
| Hard Granite (Class IV/V) | 350mm / 14" | 1,400 – 1,800 RPM | 25 – 33 m/s | 12 – 18 L/min (Wet) | Keyhole Segmented Rim |
| Marble & Soft Limestone | 300mm / 12" | 2,000 – 2,500 RPM | 32 – 40 m/s | 10 – 15 L/min (Wet) | Continuous Rim / Narrow Slot |
| Porcelain & Ceramic Tile | 115mm – 125mm / 4.5"–5" | 10,000 – 12,200 RPM | 60 – 80 m/s | Dry / Wet Dual Use | Ultra-Thin Turbo Mesh Rim |
| Reinforced Concrete & Brick | 230mm / 9" | 6,600 – 7,600 RPM | 50 – 70 m/s | Dry / Wet (Dust Control) | Aggressive Wave Turbo |
Transitioning from traditional Cobalt-heavy matrices to environmental Nickel-Iron-Copper nanograin alloys to reduce raw material volatility while increasing matrix yield strength.
Integrating 3D ordered diamond positioning (Arix technology) directly into high-pressure hot-sintering molds to ensure uniform diamond exposure and 50% longer cutting life.
Embedding composite vibration-absorbing polymesh layers inside laser-welded silent core bodies, reducing jobsite decibel noise by over 12 dB(A).
Expert technical insights regarding hot-pressed diamond saw blade selection, manufacturing standards, OEM procurement, and troubleshooting.
Hot press sintered diamond saw blades are manufactured by simultaneously applying high hydraulic pressure (15–35 MPa) and elevated temperatures (750°C–980°C) inside graphite molds. This process eliminates micro-porosity within the metallic matrix, achieving over 99.2% of theoretical metal density. In contrast, cold press blades are compacted at room temperature and then pressureless-sintered in an oven, leaving residual porosity that leads to lower diamond retention. Hot-pressed blades provide up to 35% longer service life, superior segment shear strength, and cleaner cutting edge quality on hard stones and porcelain tiles.
The golden rule of diamond tool selection is: Hard Materials require Soft Matrix Bonds; Soft Materials require Hard Matrix Bonds. Granite is an extremely hard, dense stone; therefore, a soft metal matrix bond (containing higher bronze or copper content) is required so that worn diamonds shed readily to expose new, sharp synthetic diamonds. Marble and sandstone are softer but highly abrasive; they require a hard matrix bond (containing tungsten carbide or iron powders) to resist abrasive slurry wear and hold diamonds in place longer.
Sintered stone slabs contain high internal stress from their ultra-high pressure manufacturing process. Standard continuous or coarse segmented blades can create micro-vibrations and heat concentration, triggering catastrophic slab cracking. JIAYAN's J-Slot blade geometry features narrow, curved radial slots that act as thermal expansion buffers and stress-relief channels. Water flows deep into the J-slots to flush out fine abrasive slurry instantly, keeping the cutting zone cool and guaranteeing zero-edge chipping on high-value countertop slabs.
Small diameter hot-pressed blades (105mm to 230mm) engineered with turbo or segmented rims are suitable for dry cutting on angle grinders and masonry saws. The hot-sintering process creates a heat-resistant matrix bond capable of withstanding intermittent dry thermal spikes up to 600°C. However, for continuous bridge saw cutting or blade diameters of 350mm and above, wet cutting with adequate water coolant is strictly recommended to preserve blade tension, maintain cutting accuracy, and suppress hazardous silica dust.
During high-temperature hot pressing, uncoated synthetic diamonds can suffer from graphite conversion or thermal oxidation when exposed to metal powders above 800°C. Titanium coating acts as a protective chemical barrier around the diamond crystal. Furthermore, during sintering, the titanium layer reacts with the metallic matrix to form a thin Titanium Carbide (TiC) chemical bond, increasing the diamond retention force by over 40% and drastically reducing premature diamond pull-out during heavy cutting.
JIAYAN provides complete end-to-end OEM/ODM production services. Global procurement partners can customize blade core steel thickness, diamond grit mesh size (e.g., 30/40, 40/50, 60/80), concentration, matrix alloy hardness, segment height (up to 15mm), laser-etched logos, blade color coatings, and custom retail box packaging. Sample production typically takes 7–10 days, with full container lead times within 20–25 days.
If a diamond saw blade loses its cutting speed and starts pushing material without cutting (glazing), the metal matrix has smoothed over without exposing new diamond grains. To dress or re-sharpen the blade, make 3 to 5 shallow passes through a highly abrasive material such as soft sandstone, abrasive firebrick, or an asphalt block. The abrasive block wears away the outer metal matrix layer, exposing fresh, sharp diamond points.
JIAYAN is an active enterprise member of the China Superhard Material Association. All our hot-pressed diamond cutting tools are manufactured under ISO9001:2015 quality management systems and strictly comply with the European Safety Standard EN13236 for superhard abrasive products, ensuring optimal structural safety under max RPM operating conditions.
Direct factory pricing, flexible MOQ, and standardized export packaging for worldwide distributors and stone fabricators.
Bore Size: 22.23mm / 25.4mm / 50mm
Feature: Chip-Free Fast Cutting
Diameter: 350mm (260-350mm range)
Application: Dekton & Compact Slabs
Segment Height: 12mm / 15mm
Matrix Type: Heavy-Duty Alloy
Core Type: Standard & Silent Core
Usage: Bridge Saw & Block Saw
Rim Type: Turbo / Mesh / Smooth
Application: Tile & Stone Trim
Edge Finish: Smooth Zero-Chipping
Speed: High Feed Efficiency
Slot Type: Keyhole Heat Dissipation
Application: Heavy Industrial Tiles
Kerf: 1.0mm / 1.2mm
Benefit: Fast Cut & Material Saving
Partner directly with JIAYAN Superhard Tools for wholesale pricing, custom segment formulations, white-label branding, and dedicated engineering support.


