Engineered for extreme wear resistance, chip-free edge clarity, and optimal heat dissipation across stone, ceramic, and dense composite processing.








In modern industrial fabrication, the term "Diamond Hacksaw Blade" represents both specialized linear reciprocating ultra-hard sawing blades and high-speed rotary segment discs engineered to slice through extremely tough non-ferrous, mineral, and composite matrices. As a leading China Diamond Hacksaw Blade Factory & Exporter, JIAYAN Superhard Tools leverages advanced powder metallurgy and synthetic diamond crystallographic control to overcome the traditional bottlenecks of blade wear, thermal fatigue, and edge chipping.
Global demand for superhard cutting media is shifting toward high-density materials such as sintered stones (Dekton, Neolith), ultra-compact porcelain slabs, heavy reinforced concrete, and abrasive natural quartzites. Standard steel-tooth saw blades fail almost instantly when encountering these Mohs 7+ hardness materials. By embedding High-Pressure High-Temperature (HPHT) synthetic diamond grit into precisely engineered metal alloy matrices (Cobalt-Copper-Nickel-Iron blends), our tools achieve unmatched material removal rates while retaining razor-sharp perimeter fidelity.
Optimal tool life is governed by matrix attrition matching target material abrasiveness. If the metal matrix bond is too hard, the diamonds glaze over and lose cutting action; if too soft, premature diamond drop-out occurs. JIAYAN's automated sintering controls bond density within ±0.02 g/cm³, ensuring self-sharpening efficiency across variable feed rates.
JIAYAN Superhard Materials operates as an active member of the China Superhard Material Association, holding full ISO 9001 quality system certifications and EN13236 safety compliance for high-speed diamond tooling exports.
Inside JIAYAN's cleanroom vacuum sintering center, every diamond hacksaw blade and rotary disc is formulated at the molecular level.
We source premium monocrystalline diamonds characterized by complete cubooctahedral crystal morphology. High thermal stability (Ti-coated or Ni-coated options) ensures the diamond grains do not suffer graphitization during high-temperature hot-pressing sintering stages (up to 950°C).
Depending on target application depth, JIAYAN utilizes three key routes: Hot-Pressed Sintering for continuous thin-rim ceramic blades; High-Frequency Silver Brazing for standard stone processing; and Automated Laser Welding for heavy-duty dry cutting of concrete and granite where segment detachment must be mathematically impossible.
High-end architectural processing requires low noise pollution. JIAYAN integrates multi-layer sandwich steel cores (Steel-Copper-Steel) alongside laser-cut J-slots and key-hole slot geometry to dissipate harmonic vibrations and reduce cutting noise by up to 15 dB(A).
| Blade Series / Spec | Target Workpiece Material | Segment Bond Hardness | Peripheral Speed (m/s) | Recommended Coolant Feed |
|---|---|---|---|---|
| 14" Sintered Stone Spec | Porcelain Slabs, Dekton, Neolith | Medium-Soft (Bronze-Cobalt) | 28 - 35 m/s | High Water Flow (Wet Sawing) |
| 350mm Granite Heavy Duty | Class 1 to Class 5 Natural Granite | Medium-Hard (Iron-Cobalt Matrix) | 35 - 42 m/s | Standard Water Recirculation |
| J-Slot Ceramic Series | Vitrified Tile, Glazed Ceramic | Soft (Self-Sharpening Alloy) | 30 - 40 m/s | Wet / Optional Dry Trim |
| Ultra-Thin 1.0mm Disc | Ultra-Dense Wall Tiles & Glass Mosaic | Ultra-Soft Bond Matrix | 40 - 50 m/s | Wet Cutting Precision Finish |
| Concrete & Masonry Laser Blade | Reinforced Concrete, Green Concrete | Hard (Tungsten Carbide Reinforced) | 45 - 60 m/s | Dry Cutting / Heavy Air Flow |
From Italian stone fabrication shops to North American civil infrastructure projects, JIAYAN diamond blades are optimized for local operational environments.

Used extensive in CNC bridge saws and five-axis cutting centers. Achieves perfectly straight mitre cuts (45-degree edge joints) on jumbo sintered stone slabs without edge blowout or micro-cracking.

Integrated into high-speed automated sizing lines where continuous operation demand zero downtime. Blades maintain true concentricity across millions of linear meters of cut tile.

Heavy-duty laser welded diamond circular saw blades engineered to tackle rebar-embedded concrete, asphalt road paving, and primary quarry granite block splitting under extreme ambient temperatures.
China accounts for over 80% of the world's synthetic diamond raw crystal production, centered in Henan and surrounding industrial clusters. Operating directly within this primary supply ecosystem, JIAYAN Superhard Tools eliminates multi-tier intermediary markups, providing international importers with superior performance-to-cost ratios.
Our industrial plant in Wuhu combines localized raw material access (fine metal powders, high-purity synthetic diamonds, premium steel cores) with automated German-engineered cold-pressing machines and computerized vacuum hot-sintering furnaces. This direct integration guarantees:
Whether you require standard 350mm granite blades or specialized continuous rim J-slot blades for porcelain export under your own brand name, our turnkey OEM solutions cover laser engraving, customized packaging, dynamic balance testing, and standardized palletized logistics.
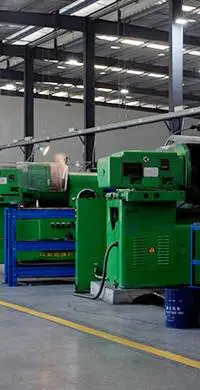
Multi-stage temperature and pressure profiling prevents diamond graphitization during matrix bond formation.
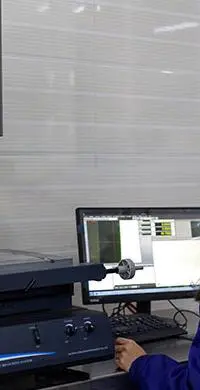
Secure anti-rust ocean packaging, air-freight fast shipping, and direct export customs clearance.
JIAYAN is investing in next-generation diamond tool technologies to meet the evolving demands of automated Smart Factories.
Chemical bonding layers applied to diamond crystals improve matrix thermal retention by 35%, extending blade life during water-scarce cutting conditions.
Transitioning from random diamond dispersion to precise 3D grid alignment within segments, maximizing cutting speed and ensuring uniform wear patterns.
Developing eco-friendly iron-copper-nickel sintered bonds to comply with strict European REACH directives while maintaining Cobalt-grade tensile toughness.
Incorporating real-time vibration signatures into automated core manufacturing to ensure sub-micron radial balance prior to factory dispatch.
Stay informed with technical research papers, quality control testing methodologies, and international exhibition reports from JIAYAN Superhard.
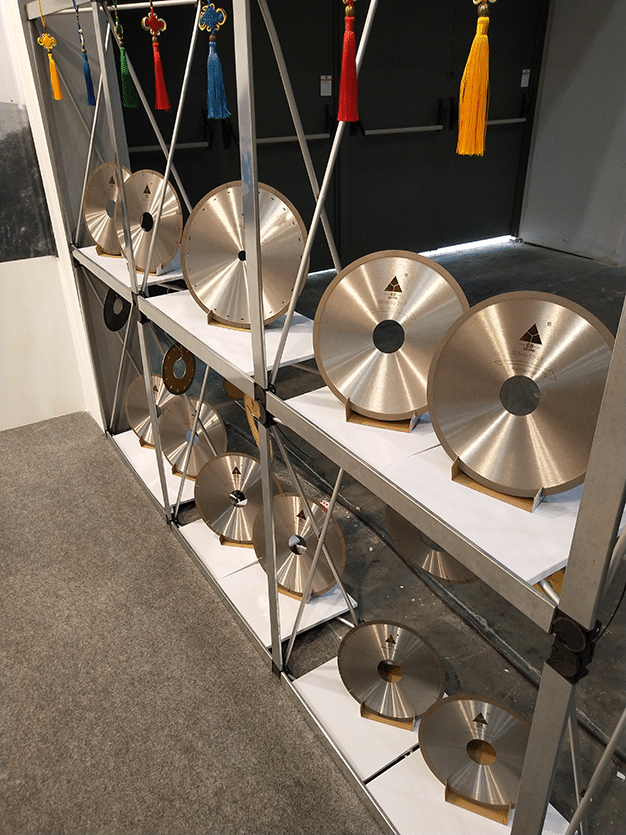 Technical Article
Key testing procedures covering non-destructive ultrasonic testing, mechanical bending moment verification, and metallurgical bond micro-analysis.
Read Full Technical Report →Showcasing ultra-thin diamond cutting discs and J-slot blades for global ceramic machinery manufacturers at the Canton Fair Complex.
View Exhibition Highlights →Presenting high-speed diamond tools and customized OEM solutions to European stone fabricators and machinery distributors.
Explore Event Summary →Explore our full range of certified diamond cutting discs, continuous rim blades, and laser-welded segments.
Expert answers addressing operating parameters, troubleshooting blade wear, and custom formula optimization.
Edge chipping occurs due to micro-vibrations and excessive bond hardness. To achieve a clean finish, select a continuous rim or J-slot blade with a soft bronze-cobalt matrix bond, ensure high water volume coolant flow, and drop your bridge saw feed rate to 1.2–2.0 m/min while maintaining high spindle speeds (2200–2800 RPM).
Silver-brazed segments use a low-melting silver alloy filler joint, which requires continuous wet cooling during operation to prevent solder reflow. Laser welding fuses the segment directly into the steel core plate at the atomic level, providing superior heat tolerance essential for safe, heavy-duty dry cutting of concrete and masonry.
Glazing occurs when the metal matrix bond is too hard for the workpiece material, causing diamond grains to wear flush without shedding to expose fresh diamond edges. You can "dress" or re-sharpen the blade by making several cuts through highly abrasive dressing sandstone or soft refractories.
Yes. We routinely engineer proprietary bond formulations matched to regional stone characteristics—such as hard Brazilian granites, abrasive Indian sandstones, or high-density European porcelain. OEM services also include custom bore dimensions, drive holes, dynamic balancing, and custom branded core art.
Every production run undergoes strict quality audits: 1) Laser weld torque testing; 2) Steel core axial and radial runout measurement (< 0.03mm threshold); 3) X-ray segment density inspection; and 4) Spindle balance dynamic testing under rated maximum operational RPMs.
For standard stock sizes (e.g., 350mm/14" discs), dispatch is available within 7 business days. Custom OEM segment manufacturing typically requires 15–25 days depending on total order volume. Flexible MOQs start at 20 units for large diameter blades and 100 units for smaller angle grinder discs.



