Engineered by JIAYAN Superhard Materials for supreme wear resistance, thermal endurance, and high-speed cutting efficiency across global industrial applications.








Analyzing the technological transition from conventional silver brazing to state-of-the-art laser metallurgical beam fusion in severe industrial environments.
Laser welding creates a direct atomic bond between the superhard diamond segment matrix and the high-strength alloy steel core. Unlike soft-soldered silver brazing, which melts at approximately 600°C to 700°C, high-energy Nd:YAG and Fiber laser beams produce a homogenous joint zone capable of withstanding extreme operational friction without thermal detachment.
Occupational safety standards across Europe, North America, and Australia strictly enforce EN13236 regulations for handheld power cutters and walk-behind floor saws. Laser-welded blades guarantee a shear strength exceeding 35-45 MPa at the joint, virtually eliminating segment loss fatalities during dry-cutting operations on reinforced concrete and hard stone.
Driven by global infrastructure modernization, mega-highway expansions, deep civil engineering, and ultra-hard engineered slab processing (Sintered Stone / Dekton), global procurement has pivoted sharply toward custom laser welded tooling. Demand for custom segment geometries (J-Slot, Keyhole, Turbo Rim) has grown by 14.8% year-over-year.
Comprehensive metallurgical performance evaluation between JIAYAN Laser Welded Blades, Silver Brazed Saw Blades, and Standard Hot-Pressed Cutters.
| Performance Metric | Laser Welded Technology (JIAYAN OEM) | Silver Brazed (Induction Soldered) | Hot-Pressed (Sintered Continuous) |
|---|---|---|---|
| Metallurgical Bond Mechanics | Deep Fusion Weld (Steel Core to Transition Zone) | Capillary Alloy Layer (Ag-Cu-Zn alloy filler) | Direct Mechanical Interlock & Sintering matrix |
| Joint Shear Strength | > 35 - 50 MPa (Exceeds EN13236 Standard) | 15 - 25 MPa (Risk of softening at high thermal load) | N/A (Integral Body Construction) |
| Maximum Thermal Resistance | 800°C - 1000°C (Full Dry Cutting Operational Safety) | 300°C - 450°C (Requires mandatory continuous water cooling) | 400°C - 600°C (Limited Dry Cutting) |
| Material Processing Versatility | Cured Heavy Reinforced Concrete, Asphalt, Granite, Quartzite | Natural Marble, Soft Sandstone, Tile (Wet Sawing) | Ceramic Tile, Porcelain Slabs, Thin Masonry |
| Core Steel Stress Tolerance | High Yield Strength 65Mn / 50Mn2 (Dynamic Laser Tensioned) | Standard Carbon Tool Steel (Medium Tension) | Standard Cold-Rolled Carbon Sheet Steel |
| Vibration & Runout Control | Radial Runout < 0.02 mm; Axial Runout < 0.015 mm | Radial Runout < 0.05 mm | Radial Runout < 0.08 mm |
Combining proprietary powder metallurgy, dynamic laser stress-relieving, and automated multi-axis robotic laser welding for international B2B buyers.
Our R&D department formulates matrix bonds utilizing premium Cobalt (Co), Nickel (Ni), Iron (Fe), and Tungsten Carbide (WC) micro-powders paired with high-grade synthetic monocrystalline diamonds (MBD and SDB series). Grit sizing from 30/40 mesh for aggressive heavy concrete cutting to 60/80 mesh for delicate, chip-free porcelain cutting ensures targeted crystal friability and wear balance.
Every steel core (65Mn spring steel alloy) undergoes computer-controlled laser tensioning to establish precise internal stress distribution. This guarantees that when the blade operates under extreme peripheral speeds (up to 80 m/s) and severe heat, the blade maintains perfect flatness without wobbling, snaking, or thermal warping.
Tailored diamond blade formulations designed to conquer diverse geographical geology, job-site machinery, and material hardness variations.
Heavy civil contractors demand extreme durability for cured concrete highway joint sawing, wall sawing, and asphalt overlay cutting. Blades are optimized with drop-segment protection to prevent core undercut caused by abrasive slurry.
Key Spec: Hard Bond / Co-Rich MatrixHigh ambient temperatures combined with ultra-dense Class IV and Class V granites (e.g., Pink Granite, Sandstone) demand highly free-cutting soft-medium metal matrices with self-sharpening diamond concentration.
Key Spec: Soft Bond / High Diamond GritRapid expansion in ultra-compact sintered stone slabs and mega-porcelain tiles requires ultra-thin continuous rim or J-slot laser blades that eliminate edge chipping while operating on high-speed CNC automated cutting tables.
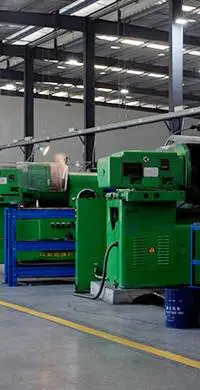
Key Spec: J-Slot / Ultra-Thin RimLocated in Wuhu, Anhui Province, China, JIAYAN Superhard is an industry-leading manufacturer of diamond saw blades, circular cutting discs, and superhard tooling solutions. As an active official member of the China Superhard Material Association, our production lines combine state-of-the-art automated laser welding equipment with rigorous metallurgical quality testing.
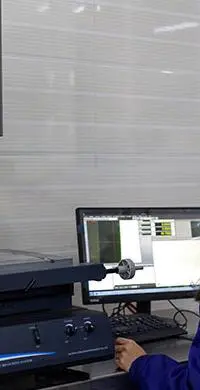
Every production batch undergoes 100% torque shear testing, ultrasonic flaw detection at the weld seam, and dynamic balance calibration. We provide worldwide OEM/ODM manufacturing, private label packaging, custom segment engineering, and flexible MOQ options for industrial buyers, distributors, and equipment brand owners.



Strategic engineering developments defining the next decade of industrial cutting efficiency, environmental sustainability, and precision automation.
To mitigate thermal graphite transformation during sintering and laser beam exposure, JIAYAN is pioneering chemical vapor deposition (CVD) titanium coatings on synthetic diamond crystals. This micro-layer prevents thermal oxidation and increases diamond retention strength within the metal matrix by over 30%.
Integrating real-time infrared pyrometers into our robotic fiber laser welding stations allows instantaneous adjustment of laser energy density ($10^6 \text{ W/cm}^2$). This eliminates micro-porosity at the weld seam, yielding unmatched shear consistency across large-scale manufacturing runs.
Urban construction noise standards require acoustic suppression. Next-generation laser welded blades feature laser-etched dampening slots filled with viscoelastic copper/resin damping compounds, reducing operational cutting noise by up to 12 dB(A).
In response to global raw material sustainability initiatives, our laboratory has engineered ultrafine nanocrystalline Iron-Bronze-Tungsten (Fe-Cu-WC) matrix systems that replace cobalt without compromising segment wear life or diamond retention.
Expert engineering insights regarding laser-welded diamond blade selection, operational safety, matrix matching, and OEM procurement.
Explore our complete catalog of certified diamond cutting discs and custom laser welded saw blades. Direct factory export with worldwide delivery.
Request customized technical quotes, material sample testing, private-label OEM catalogs, or factory audit information directly from our engineering team.



