
How to Detect the Welding Strength of Laser Welding Diamond Saw Blades
Understanding key inspection methods for laser-welded joints—covering microstructural evaluation, torque testing, and non-destructive ultrasonic shear inspection.
Precision-engineered diamond cutting discs manufactured with advanced sinter powder metallurgy and laser-welded joint integrity for global B2B procurement.








In modern industrial stone fabrication and high-volume ceramic slab manufacturing, the transition toward ultra-compact materials—such as sintered stone slabs (e.g., Dekton, Neolith), high-density engineered quartz, and vitreous porcelain—has completely redefined requirements for cutting tool performance. Standard dry-cutting or generic diamond saw blades consistently succumb to catastrophic segment micro-fracturing, thermal graphitization, edge chipping, and core tension degradation.
As a leading Custom Wet Cutting Diamond Saw Blade Factory & OEM Manufacturer based in Wuhu, China, JIAYAN Superhard Tools engineered this technical guide to dissect the underlying material physics, powder metallurgy formulations, fluid cooling dynamics, and Industry 4.0 manufacturing processes that drive modern superhard cutting tools.
By leveraging synthetic diamond micro-crystallites synthesized under extreme High-Pressure High-Temperature (HPHT) environments, combined with tailored Cobalt-Bronze-Iron sintered matrix bonds, JIAYAN blades achieve an optimal balance between matrix self-sharpening (wear rate matching) and diamond retention strength. Explore our specialized Diamond Saw Blade For Stone Series to evaluate customized blade options for bridge saws, CNC cutting centers, and manual radial cutters.

Analyzing the interaction between synthetic diamond crystal degradation, matrix erosion rates, and coolant dynamic fluid delivery in wet cutting operations.
The cutting efficiency of a wet saw blade is dictated by synthetic diamond grit quality. JIAYAN utilizes premium SDA/MBD grade synthetic diamonds featuring high thermal stability (TTS) and controlled micro-fracturing characteristics.
For hard granite and sintered porcelain, grit size ranges from 40/50 mesh to 60/80 mesh. Finer grit spreads the cutting load across more active diamond points, virtually eliminating edge chipping on brittle ceramic glazes.
The metal bond matrix holds the diamond grains until they become dull, releasing them to expose fresh sharp crystal edges. JIAYAN formulates complex multi-element matrices utilizing Cobalt (Co), Nickel (Ni), Copper (Cu), and Iron (Fe) powders.
By employing vacuum hot-pressing sintering at 850°C–980°C, our segments achieve precise density (>99.2% theoretical density), preventing premature diamond pull-out under severe tangential forces.
Wet cutting is not merely about temperature suppression; it is a critical swarf transport mechanism. Water acts as a hydrodynamic carrier flushing slurry out of the kerf, preventing thermal shock cracking of the steel core.
Our engineered J-Slot and Keyhole slot geometry enhances water penetration directly into the cut zone, eliminating boundary layer thermal resistance and maintaining temperatures below 200°C to prevent diamond graphitization.

As a verified member of the China Superhard Material Association, JIAYAN operates an integrated Industry 4.0 production facility equipped with automated cold-pressing, vacuum hot-sintering, high-frequency induction brazing, and fully automated laser welding units.
Every wet diamond saw blade core undergoes strict mechanical tensioning and computerized dynamic balance calibration. Core tensioning ensures that under operational RPM (typically 1400 to 2900 RPM depending on diameter), centrifugal force and heat expansion offset each other, keeping radial runout strictly within <0.02 mm and axial wobble virtually zero.
Learn more about our strict manufacturing protocols in our Technical Blog Insights, detailing advanced testing procedures such as non-destructive ultrasonic segment inspection and laser weld torque strength verification.
Different structural substrates demand dedicated matrix hardness, diamond grit concentration, and slot edge designs. JIAYAN provides tailored OEM blade solutions.
Material Challenge: Highly compressed glass-ceramic matrices with high internal stress. Standard blades cause edge blowout or instant slab cracking upon relief of internal tension.
JIAYAN Solution: Our 14 Inch Sintered Stone Blade incorporates soft, wear-free bronze-cobalt bonds combined with micro-fine 60/80 grit diamonds. J-slot vibration isolation channels absorb mechanical harmonics, delivering factory-clean miter joints without chipping.
Material Challenge: Quartz content exceeding 70% with high abrasive index (Mohs Hardness 7+), causing severe friction wear on blade matrix and rapid diamond dulling.
JIAYAN Solution: Engineered with ultra-hard iron-nickel matrix alloys and high-density 30/40 mesh diamonds. Our 350mm Granite Saw Blade features reinforced keyhole segments, maximizing linear feed speeds (up to 3.5 m/min on bridge saws).
Material Challenge: Fragile glazed surfaces requiring precise zero-tolerance kerf width without surface micro-fracturing or glaze chipping.
JIAYAN Solution: Continuous rim and ultra-thin 1.0mm/1.2mm diamond cutting discs. Hot-pressed continuous diamond rims create smooth hydrodynamic fluid action, allowing clean cutting at high spindle speeds.
Material Challenge: Soft but sticky, non-abrasive material (Mohs Hardness 3-4) that glazes over standard hard-bond blades due to inadequate matrix wear.
JIAYAN Solution: Specifically formulated hard-bond matrices with aggressive diamond concentration that maintain continuous exposure of diamond crystal edges without clogging or load buildup.
Comprehensive engineering parameters for industrial distributors, machine manufacturers, and stone processing plant procurement directors.
| Blade Diameter (mm/inch) | Inner Bore / Arbor (mm) | Segment Specs (L x W x H mm) | Diamond Mesh Size | Optimal Operating RPM | Recommended Feed Rate | Target Substrates |
|---|---|---|---|---|---|---|
| 250mm / 10" | 50mm / 60mm / 25.4mm | 40 x 2.2 x 10 / 12mm | 50/60 – 60/80 Mesh | 2400 – 2800 RPM | 1.2 – 2.0 m/min | Porcelain, Ceramic, Thin Sintered Stone |
| 300mm / 12" | 50mm / 60mm | 40 x 2.8 x 10 / 15mm | 40/50 – 50/60 Mesh | 1800 – 2400 RPM | 1.5 – 2.5 m/min | Sintered Stone, Marble, Engineered Quartz |
| 350mm / 14" | 50mm / 60mm | 40 x 3.2 x 15 / 20mm | 35/45 – 40/50 Mesh | 1400 – 2100 RPM | 2.0 – 3.5 m/min | Granite, Hard Quartzite, Sintered Slab |
| 400mm / 16" | 50mm / 60mm | 40 x 3.6 x 15 / 20mm | 30/40 – 40/50 Mesh | 1200 – 1800 RPM | 2.0 – 4.0 m/min | Heavy Granite Blocks, Concrete, Quartzite |
Noise-reduction sandwich cores consisting of two steel sheets laminated with a sound-dampening copper layer. Reduces operational noise by 10 to 15 dB while preventing core resonance vibration.
We offer both high-frequency silver-brazed segments for standard stone cutting and 100% automated laser-welded segments for maximum joint safety under severe thermal shear stresses.
Complete OEM services including custom laser engraving of blade parameters, bespoke color coating, custom arbor bushing adaptations, and drop-ship retail packaging for global brands.
Combining competitive direct factory cost structures with uncompromised metallurgical quality control.
100% batch inspection of synthetic diamond powders, cobalt alloys, and high-tensile 75Cr1 steel cores to ensure consistent hardness and metallurgical purity.
Automated powder mixing and hot-press sintering lines enable flexible production scheduling with lead times under 15 days for full container orders.
Strict safety adherence governing European standard shear resistance, spin testing up to 1.5x maximum RPM, and axial tension verification.
Direct export from Shanghai/Ningbo ports with full customs compliance documentation, MSDS, Certificate of Origin, and localized technical support.
Pioneering next-generation abrasive technologies for ultra-hard synthetic materials and green powder metallurgy.
Integrating chemical vapor deposition (CVD) titanium-coated diamond crystals. The metallic Ti coating forms a chemical bond with the matrix during sintering, increasing diamond retention force by over 35% and preventing early thermal graphitization.
Developing environment-safe, cobalt-free iron-copper-nickel sintered matrices. These advanced green alloys match cobalt matrix toughness while significantly mitigating raw material price volatility and meeting strict European environmental directives.
Utilizing algorithmic spectroscopy analyzing stone specimen composition (calcium carbonite vs. silica content) to automatically specify tailor-made segment bond formulations for custom OEM industrial orders.
Addressing key operational concerns, trouble-shooting scenarios, and technical specs for stone fabricators and tooling distributors.
Stay informed with technical developments, testing methodologies, and international tradeshow participation from JIAYAN Superhard.
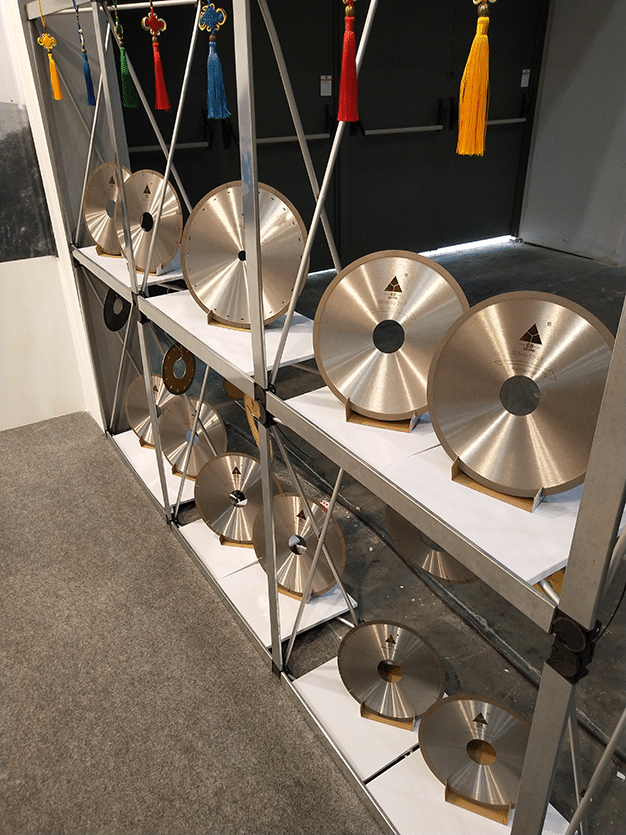
Understanding key inspection methods for laser-welded joints—covering microstructural evaluation, torque testing, and non-destructive ultrasonic shear inspection.
Showcasing our continuous rim J-slot ultra-thin blades at Guangzhou Canton Fair Complex for global ceramic plant operators.
Demonstrating high-speed porcelain slab cutting solutions to European machinery manufacturers and distribution partners.
Select your operational parameters or request customized factory specifications directly from our engineering team.
Direct factory engineering support, OEM custom arbor & bond formulations, and strict EN13236 compliance testing. Request a detailed engineering catalog or sample blade today.


