Engineered for high-feed bridge saws, automatic line cutters, angle grinders, and high-precision CNC edge-profiling machinery. Verified dynamic balance and high-density diamond matrix retention.








The global stone, ceramic, and construction abrasive cutting disc market is undergoing a structural technological transition. Driven by the mass adoption of ultra-compact surfaces—such as sintered porcelain slabs (e.g., Neolith, Dekton), ultra-hard engineered quartzites (Mohs hardness 7–8), and heavily reinforced high-performance concrete—conventional electroplated and low-temperature sintered saw blades are rapidly being phased out.
Modern fabrication facilities demand circular diamond saw blades capable of maintaining an ultra-clean kerf profile at high linear traverse rates (3.0–6.0 m/min) while eliminating micro-chipping, segment loss, and thermal deflection. As a recognized member of the China Superhard Material Association, JIAYAN Superhard leverages advanced powder metallurgy, multi-stage hot isostatic pressing (HIP), and automated laser welding to redefine standard diamond blade tool lifespans and edge precision.

For global tile distributors, large-scale masonry contractors, and stone processing conglomerates, the initial purchase price of a diamond saw blade represents less than 15% of the total cutting cost per square meter. The dominant cost drivers are downtime caused by frequent tool changes, material scrap rates from edge chipping, and power consumption during high-drag operation.
Optimizing diamond crystal grade (high-tensile synthetic diamonds with Ti/Cr coatings) and cobalt-based matrix hardness ensures continuous, steady diamond self-sharpening without premature pull-out or glazing, lowering effective cost per square meter processed by 32% compared to standard aftermarket blades.
Laser-cut core bodies manufactured from 75Cr1 and 65Mn spring steels undergo heat treatment to 40–44 HRC. Precision tensioning guarantees maximum rigidity, preventing blade wobble and wandering under automated CNC feed pressures up to 6,000 mm/min.
High-value sintered porcelain slabs (12mm–20mm thickness) exhibit immense internal firing tension. Our specialized J-slot and key-slot continuous rim configurations provide localized thermal dissipation and micro-vibration damping to eliminate secondary edge-finishing steps.
| Evaluation Parameter | Standard Low-Cost Blade | JIAYAN Sintered Industrial Grade | JIAYAN Laser-Welded Bridge Saw Grade | Operational Impact |
|---|---|---|---|---|
| Diamond Crystal Mesh | MBD4 (Standard Frangible) | SMD30/40 Coated Synthetic | High-Strength Monocrystalline (SMD50+) | +45% Wear Resistance |
| Matrix Bond Metallurgy | Basic Iron-Bronze Alloy | Cobalt-Nickel Ultra-Dense Alloy | Tungsten Carbide-Cobalt Hot Isostatic Pressed | Zero Segment Stripping Risk |
| Dynamic Runout Tolerance | < 0.25 mm | < 0.08 mm | < 0.04 mm | Zero Edge Spalling on Porcelains |
| Linear Feed Rate (Granite Class 4) | 1.2 – 1.8 m/min | 2.5 – 3.8 m/min | 4.5 – 6.2 m/min | 2.5x Production Output |
| Safety Compliance Standard | Uncertified / Basic | EN 13236 Standard Compliant | EN 13236 / OSA Certified Joint Strength | Operator Safety & Legal Protection |
The manufacturing excellence of diamond cutting saw blades lies at the intersection of thermal thermodynamics, metallurgical crystal bonding, and high-frequency acoustic tension balancing.
Synthetic diamonds are coated with nanometric titanium layers to prevent diamond thermal graphitization at temperatures above 700°C during hot-pressing.
Pre-alloyed metal powders (Co, Cu, Ni, Sn, WC) are sintered under precise isostatic hydraulic pressure (30–35 MPa) at isothermal holding states to achieve 99.8% theoretical density.
High-power Nd:YAG and fiber laser welding beams fuse the diamond segment transition layer into the hardened steel core, achieving full weld penetration without micro-porosity.
Each blade core undergoes specialized roller-tensioning and dynamic balancing tests to counteract radial expansion caused by centrifugal and thermal loads during high-speed rotation.
In accordance with our published research ("How to Detect the Welding Strength of Laser Welding Diamond Saw Blades"), every batch of heavy-duty segmented blades undergoes three-tier destructive and non-destructive testing: appearance inspection of the transition weld seam under 50x optical magnification, metallurgical microstructure phase boundary evaluation, and 100% torsional bending torque tests exceeding European EN 13236 safety thresholds by 25%.

Computer-monitored heating curves eliminate internal thermal stresses within the diamond segments.

Laser axial runout verification ensures cutting accuracy to within +/- 0.02 mm across diameter lines.
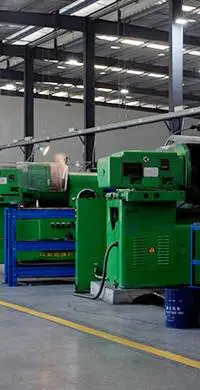
Monthly capacity exceeding 150,000 diamond discs for global distributor supply chain safety.
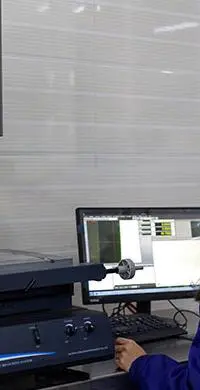
Custom laser marking, silent sandwich core options, and specialized packaging for brand partners.
Cutting tools are not universal; metallurgical bonding matrices must be calibrated to match the specific abrasive properties and Mohs hardness of the workpiece.
Challenge: Vitrified surfaces with high internal stress; prone to corner breakout, edge shelling, and blade clamping.
Solution: 14" (260-350mm) specialized blades with soft cobalt-bronze matrix bonds, ultra-fine diamond mesh (100/120#), and continuous key-hole water gullets for smooth cutting.
Challenge: Extremely abrasive high-quartz content rapidly erodes soft matrix bonds, causing premature segment wear.
Solution: Segmented sandwich circular blades (350mm–500mm) incorporating Tungsten Carbide reinforcement with alternating high-density diamond distribution for consistent cutting speeds.
Challenge: Demands 100% chip-free cut edges for seamless 45-degree miter joints on polished surfaces.
Solution: 1.0mm–1.2mm ultra-thin continuous rim discs with hot-pressed J-slots to maximize coolant evacuation and eliminate chipping.
JIAYAN actively participates in tier-one international industrial trade fairs, demonstrating technical innovations and securing strategic partnerships with distributors worldwide.
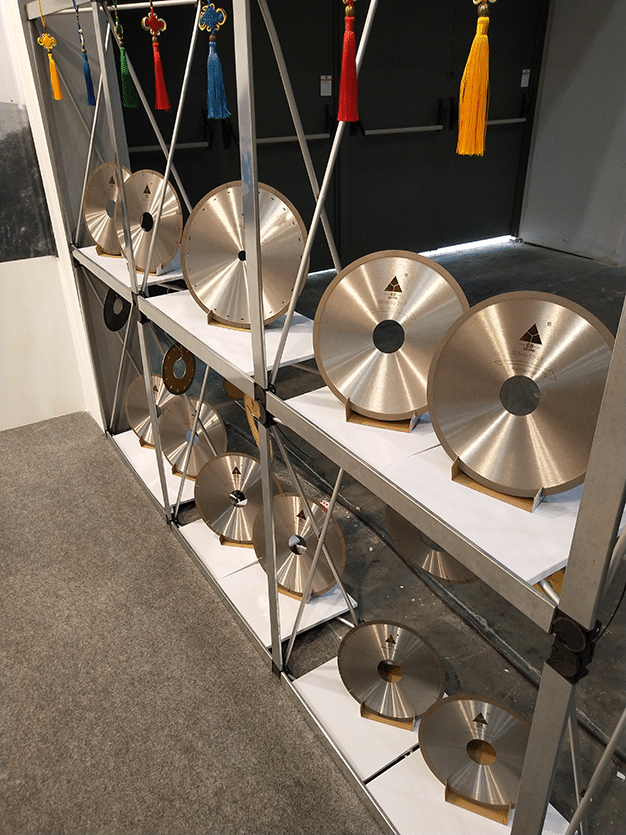
Showcased our ultra-thin diamond continuous blades and high-speed CNC bridge saw blades to major European ceramic processing machinery builders and distributors.
Presented next-generation sintered stone cutting solutions, introducing segmented J-slot silent core discs to global buyers across 40+ countries.
Anticipating the requirements of Industry 4.0 automated processing plants, our R&D team is developing cutting technologies designed for higher thermal stability and extended blade life.
Transitioning from random diamond powder distribution to precise 3D-oriented diamond micro-matrices (Arix technology), ensuring every diamond crystal engages the workpiece at optimal cutting angles for up to 50% faster cutting speeds.
Developing advanced Fe-Cu-Ni-P nano-crystalline matrix binders that match or exceed cobalt-rich bonding strength while complying with international environmental and occupational safety regulations.
Utilizing dual-steel sheets with an intermediate copper-damping foil to reduce cutting resonance below 82 dB(A), protecting operators and reducing micro-vibrations for cleaner edge quality.
Detailed engineering answers addressing real-world machine setup, feed parameters, blade glazing, and safety standards.
Select a high-performance cutting blade SKU below to request technical drawings, MOQ terms, and factory-direct volume pricing.
Connect with JIAYAN Superhard application engineers to receive custom segment matrices tailored to your regional stone hardness, arbor specifications, and cutting speeds.



