Engineered for high-RPM precision bridge saws, angle grinders, and automated CNC tile fabrication machinery.








The global abrasive and superhard cutting tools sector is undergoing a profound paradigm shift driven by architectural innovations in large-format sintered porcelain, dense quartzites, and ultra-thin ceramic slabs. In this evolving industrial landscape, sourcing from a specialized High-Quality Super Thin Diamond Saw Blade Company has transitioned from an operational preference to a strategic imperative for stone fabricators, ceramic processing plants, and commercial contractors worldwide.
Traditional diamond blades, characterized by kerf thicknesses ranging between 2.2mm and 3.5mm, exert extreme mechanical pressure and high lateral friction upon brittle substrates. When applied to high-value engineered slabs like Neolith, Dekton, Lapitec, or dense natural granite, conventional blades generate micro-fractures, edge blowouts, and unacceptable scrap rates. Super thin diamond saw blades—featuring core thicknesses reduced to as low as 0.8mm to 1.4mm—solve these structural challenges by drastically diminishing the diamond-to-substrate contact zone, reducing cutting torque, and mitigating heat accumulation.
SEO & Sourcing Insights for Procurement Directors: Modern high-speed CNC bridge saws and hand-held tile cutters demand blades with optimized matrix wear balance. Choosing certified manufacturers capable of vacuum hot-pressing and laser-tensioning ensures low-vibration cuts, extended wheel longevity, and direct cost savings per linear meter cut.
Driven by strict acoustic/dust emissions regulations and high labor costs, fabricators prioritize high-feed-rate, continuous-rim J-slot super thin blades that minimize secondary hand-polishing and edge refinishing.
Rapid infrastructure development across China, India, and Southeast Asia relies on OEM and ODM factories delivering high-volume, cold/hot-pressed turbo thin discs optimized for hard porcelain tiles and architectural granite.
High demand for massive marble slabs and intricate 45-degree miter joints requires specialized diamond grit bond formulations capable of cutting non-porous materials without thermal discoloration.
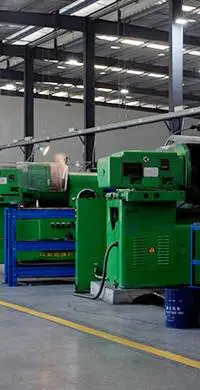
The manufacturing physics behind high-performance super thin diamond blades relies on achieving an optimal matrix wear rate that matches the friability and micro-fracturing of synthetic diamond particles. As a leading manufacturer, JIAYAN Superhard Tools utilizes state-of-the-art sintering technology to engineer ultra-thin profiles without sacrificing structural rigidity.
Continuous-rim and turbo segment diamond saw blades are produced via precise thermal-pressing routines. Hot-press vacuum sintering subjects cobalt, bronze, nickel, and iron powder matrices to high temperatures (~900°C–1050°C) under hydraulic pressures up to 35 MPa. This dense metallurgical bond prevents premature diamond pull-out, enabling micro-thin segments (1.0mm–1.4mm) to maintain structural integrity even under high feed speeds.
The core steel substrate serves as the mechanical backbone of any circular saw blade. Ultra-thin cores (0.8mm–1.0mm) are prone to thermal expansion, lateral flexing, and resonant harmonic flutter. High-end blade companies utilize imported German 75Cr1 or 65Mn spring steel cores subjected to computerized laser tensioning. This process introduces localized compressive stresses into the core, guaranteeing planar flatness within 0.02mm during high-RPM rotation.
Super thin continuous-rim blades frequently incorporate specialized laser-cut slots (such as J-Slots, Keyhole slots, or Fish-hook geometry). These structural cutouts break harmonic vibration standing waves, provide expansion relief during intense thermal friction, and facilitate localized coolant delivery directly into the cutting kerf.
| Blade Parameter | Standard Circular Saw Blade | High-Precision Super Thin Blade | Performance Benefit |
|---|---|---|---|
| Kerf Width (mm) | 2.2mm – 3.2mm | 0.8mm – 1.2mm | Reduces raw material waste by 40-60% per cut |
| Core Tensile Steel Grade | Standard 50Mn / 65Mn | High-Grade Laser Tensioned 75Cr1 | Eliminates high-speed blade wobble and flex |
| Diamond Grit Quality | Standard Synthetic MBD-4 | High-Purity Monocrystalline (Ti-Coated) | Prevents graphitization & ensures crisp edges |
| Segment Rim Geometry | Standard Block Segment | Mesh Turbo / Continuous J-Slot Rim | Ultra-smooth chip-free edges on fragile stone |
| Power Consumption | High Load (100%) | Low Load (60-70%) | Reduces motor fatigue on CNC & manual equipment |
Context: Architectural kitchen island fabrication utilizing 12mm thick Dekton slabs in high-end European and US workshops.
Solution: Operating a 14-inch (350mm) continuous J-Slot super thin diamond saw blade with a 1.2mm core and soft bronze-cobalt bond matrix. Wet cutting at 2,400 RPM with 2.5 m/min feed speed guarantees 45-degree miter seams without bottom blowout.
Context: Commercial interior wall cladding installations requiring 6mm thick large-format porcelain slabs cut on-site.
Solution: Portable angle grinders fitted with 115mm/125mm continuous mesh-turbo ultra-thin cutting discs (1.0mm thickness). High RPM dry cutting yields clean, factory-grade smooth edges without micro-cracking.
Context: High-volume stone processing plants cutting abrasive Indian black granite and Brazilian quartzite tiles.
Solution: 350mm high-segment laser-welded thin blades formulated with iron-copper matrices and titanium-coated diamond grit, maximizing linear cutting length while maintaining low noise output.
As ceramic manufacturing technologies evolve toward thinner yet denser materials (such as 3mm ultra-flexible architectural ceramics), the super thin diamond saw blade industry is entering a new era of nano-engineering and smart manufacturing. Below is the multi-year technology roadmap adopted by premier diamond tool producers:
Integration of chemical vapor deposition (CVD) diamond coatings on ultra-thin blade rims to lower friction coefficients, reduce cutting temperatures by up to 30%, and extend diamond grit exposure lifespans during high-friction operations.
Transitioning from pure cobalt powder matrix formulations to sustainable green alloys (iron-nickel-copper micro-alloys) to meet European REACH environmental standards while maintaining superior diamond hold-strength.
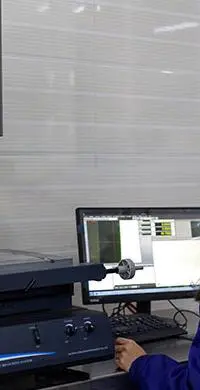
Deployment of inline optical laser sensors during factory production to inspect 100% of blade cores for dynamic balance, runout tolerance, and axial deflection, ensuring sub-micron precision for industrial OEM buyers.
Maximizing the efficiency of a super thin diamond saw blade requires precise synchronization between machine parameters, diamond matrix composition, and coolant dynamics. Operating a thin blade under improper RPM or excessive feed pressure causes blade deflection ("wandering"), rapid diamond glazing, or premature rim destruction.
| Blade Diameter | Material Target | Optimal RPM Range | Feed Rate (m/min) | Coolant Strategy |
|---|---|---|---|---|
| 115mm - 125mm (4.5" - 5") | Ceramic Tile / Porcelain Slab | 10,000 – 12,000 RPM | 1.5 – 3.0 m/min | Dry / Light Water Mist |
| 230mm (9") | Hard Marble & Granite Tiles | 5,500 – 6,500 RPM | 2.0 – 3.5 m/min | Continuous Wet Flow |
| 300mm - 350mm (12" - 14") | 12mm/20mm Sintered Stone | 1,800 – 2,400 RPM | 1.2 – 2.5 m/min | High-Pressure Dual Water Jet |
Troubleshooting Blade Glazing: If cutting speed slows dramatically and sparks appear during wet cutting, the blade matrix has become "glazed" (diamond edges worn flush with the metal bond). Refresh the blade rim by performing several passes through an abrasive dressing brick or soft sandstone block to re-expose fresh diamond grit.
In-depth technical answers addressing common inquiries from industrial buyers, equipment operators, and procurement specialists.
Direct factory supply with worldwide shipping, OEM branding, and certified ISO production quality control.

Founded in Wuhu, China, JIAYAN Superhard is a premier manufacturer specializing in diamond saw blades, ultra-thin cutting discs, and high-performance superhard tools for the global stone, ceramic, and granite processing industries. As an official member of the China Superhard Material Association, JIAYAN combines proprietary hot-pressing sintering technology with rigorous ISO-certified quality assurance.
With over a decade of international export expertise, JIAYAN provides comprehensive OEM/ODM manufacturing services, customized matrix formulations, and responsive global technical support for distributors across Europe, the Americas, the Middle East, and Southeast Asia.


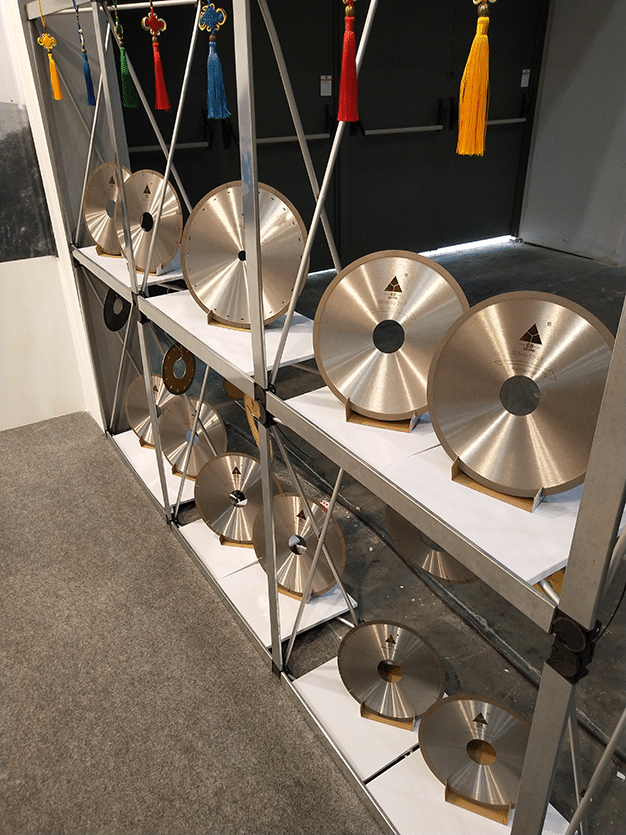
JIAYAN Superhard actively presents advanced superhard cutting innovations at international trade fairs and publishes engineering white papers on blade integrity testing:
Analysis of destructive bending tests, microscopic shear joint inspections, and metallographic analysis for laser-welded diamond blade safety standards.
Showcasing continuous mesh-turbo micro-kerf diamond blades to top European porcelain slab machinery manufacturers.
Demonstrating high-speed automated cutting solutions for 3mm–20mm ultra-thin sintered stone panels at Canton Fair Complex, Guangzhou.



