Engineered for maximum thermal resilience, zero edge-chipping, and high linear cutting velocity across sintered stone, porcelain, ceramic, and hard granite.
Analyzing Matrix Bond Degradation, Thermal Dissipation Physics, and Micro-Encapsulation Technology in Modern Superhard Tool Manufacturing.
In modern industrial stone processing and construction material fabrication, the operational shift from wet cutting to dry diamond cutting presents severe mechanical and thermal challenges. Without continuous water delivery to cool the saw blade core and flush swarf out of the kerf, cutting friction raises interface temperatures at the diamond segment tip past 800°C. Under these harsh conditions, standard diamond tools suffer from premature thermal oxidation, cobalt matrix degradation, dynamic arbor warp, and catastrophic diamond crystal pull-out.
As a specialized ODM Dry Cutting Saw Disc Manufacturer & Engineering Company, JIAYAN Superhard Materials Co., Ltd. resolves these failure modes through advanced metallurgical design and precision vacuum sintering. By synthesizing high-grade synthetic diamond grains with protective titanium coatings and combining them with custom cobalt-bronze matrix powders, our ODM engineering team delivers dry cutting circular saw discs that maintain structural integrity, sharp cutting edges, and low power consumption even under extreme continuous stress.
Dry diamond saw discs do not rely on external liquid for heat removal. Cooling depends on internal thermal conductivity through the steel core, forced convection generated by laser-cut slot expansion geometry (J-Slots and Keyhole slots), and controlled self-sharpening matrix wear rates. Our proprietary bond formulation balances diamond retention strength against micro-wear, allowing worn diamond crystals to fracture predictably while exposing fresh cutting edges.
Pioneering multi-layered matrix formulations, eco-compliant alloy binders, and high-frequency laser welding standardizations.
Thermal graphitization at temperatures above 700°C degrades synthetic diamond into graphite. JIAYAN applies a uniform titanium coating via chemical vapor deposition (CVD) to micro-encapsulate each diamond crystal. This Ti-layer creates a chemical bond between the diamond surface and metal matrix, improving diamond holding force by 35% and preventing early diamond pop-out during high-load dry cutting.
Using computer-controlled vacuum hot-press sintering equipment, we introduce controlled micro-porosity within the sintered matrix. These micro-voids trap fine stone dust particles and act as heat-dissipation micro-channels, lowering heat buildup at the kerf zone and protecting the 75Cr1 high-carbon alloy steel center from dynamic thermal warping.
Standard circular blades overheat when run dry continuously. Our ODM designs incorporate computer-modeled laser expansion slots—such as keyholes, J-slots, and helical V-gaps. These slots absorb circumferential thermal expansion, damp acoustic vibration, and force ambient air through the cutting kerf to pull away heat.
For high-risk industrial dry-cutting applications, conventional silver soldering fails as temperatures spike. JIAYAN utilizes automated high-power fiber laser welding lines. Deep-penetration laser welds fuse the metal matrix segment directly to the alloy steel blade body, yielding seam shear strengths over 600 MPa and eliminating segment loss risks under high operating speeds.
Explore JIAYAN Superhard Tools state-of-the-art facility, automated sintering lines, and precision testing labs.

Wuhu, China manufacturing facility equipped with advanced vacuum sintering presses.

Strict atmospheric controls ensure optimal alloy matrix density and grain distribution.

100% dynamic balance testing, radial deflection checks, and laser weld inspection.
Custom ODM solutions engineered for diverse stone hardness levels, high-abrasions, and delicate surface finishes.
Material Properties: Mohs Hardness 7–8, near-zero water absorption (<0.1%), extreme internal material tension.
OEM Solution: Continuous turbo-rim mesh blades and J-slot discs featuring ultra-fine diamond mesh (170/200 mesh) and soft cobalt-bronze matrix bonds. Our 1.0mm to 1.2mm kerf discs reduce lateral friction, preventing edge chipping and micro-cracking along cut lines on Dekton, Neolith, and Laminam slabs.
Material Properties: High quartz concentration, uneven quartz grain distribution, extreme mineral abrasion.
OEM Solution: Laser-welded segmented dry saw discs with high diamond concentrations (30%–35%) and tungsten-carbide reinforced matrix alloys. Designed for handheld angle grinders and masonry cut-off saws operating at linear speeds of 40–60 m/s without cooling water.
Material Properties: Brittle surface glaze, prone to surface spalling under impact.
OEM Solution: Hot-pressed continuous rim saw blades with integrated copper plugs for noise and vibration reduction. Ultra-thin core design reduces kerf loss, delivers clean top-edge cuts, and minimizes dust generation during dry installation tasks.
Material Properties: Cured reinforced concrete, asphalt over concrete, masonry block walls in water-restricted job sites.
OEM Solution: Heavy-duty keyhole slot laser-welded dry cutting discs (300mm–350mm). Deep segment gullets rapidly purge slurry and dust while drop-segment protection prevents blade body undercut wear when cutting abrasive substrates.
Comparative technical specifications for JIAYAN ODM dry cutting diamond saw blade formulations.
| Blade Series / Target Substrate | Diameter Range | Matrix Bond Composition | Diamond Grit (Mesh) | Segment Weld Type | Max RPM / Operating Velocity | Recommended Dry Cut Depth |
|---|---|---|---|---|---|---|
| Sintered Stone Special (Dekton/Neolith) | 260mm – 350mm | Soft Cobalt-Bronze Alloy | 170 / 200 Mesh | Laser Welded / Hot Press | 4,400 RPM (55 m/s) | 10mm – 20mm (Pass) |
| J-Slot Turbo Ceramic & Tile Disc | 105mm – 230mm | Medium-Soft Nickel-Bronze | 140 / 170 Mesh | Hot-Press Vacuum Sintered | 13,300 RPM (80 m/s) | Full Tile Thickness |
| Granite & Hard Natural Stone Series | 230mm – 350mm | Hard Iron-Tungsten Matrix | 40 / 50 Mesh | Automated Laser Welded | 6,600 RPM (70 m/s) | 25mm – 40mm (Pass) |
| Ultra-Thin 1.0mm Porcelain Disc | 115mm – 125mm | Ultra-Dense Micro-Matrix | 200 / 230 Mesh | Hot-Press Sintered | 12,200 RPM (80 m/s) | Fine Trim / Mitre Cuts |
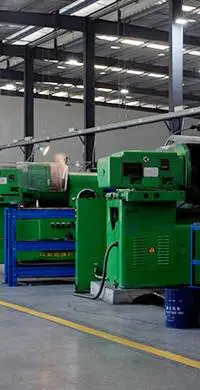
Capable of producing over 300,000 diamond discs monthly to supply worldwide distributors.
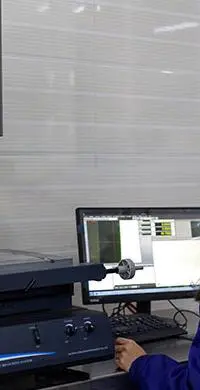
Integrated logistics support serving major industrial buyers across Europe, Americas, and Asia.
Leveraging direct superhard raw material clusters, automated production lines, and strict quality control.
Situated in China's primary superhard material industrial hub, JIAYAN maintains direct access to top-tier synthetic diamond crystallizer foundries and high-purity metal powder suppliers. This localized supply ecosystem eliminates raw material lead times and ensures price stability for large-volume OEM procurement.
From initial metal powder blending, diamond concentration verification, cold press compacting, vacuum sintering, and automatic segment grinding to laser beam welding, tension setting, and dynamic balancing—every step occurs in-house under single-roof management.
Every single dry cutting disc undergoes dynamic balance inspection on automated testing rigs. We hold dynamic runout tolerances to within ±0.03mm. This precise balancing reduces tool chatter, protects power tool spindles from wear, and ensures clean, vibration-free cuts.
From substrate hardness analysis to high-speed batch manufacturing, our engineering team manages your tool line end-to-end.
We evaluate your customer’s targeted cutting materials (e.g., specific sintered stone brands, high-silica granite, vitrified tile) and operational parameters (RPM, hand tools vs. bench saws).
Our metallurgists formulate custom metal powder blends (Cobalt, Bronze, Iron, Nickel, Tungsten) and determine optimal diamond mesh sizes, concentrations, and cooling slot geometries.
Rapid sintering of prototype discs followed by destructive testing—including 10,000+ RPM speed burst testing, segment shear tests (>600 MPa target), and cut-speed benchmarking.
Scalable high-volume production, precise laser-etched logos, arbor size adapters, custom color coatings, blister or color box packaging, and global logistics support.
Track JIAYAN Superhard Materials latest technology releases, academic papers, and international trade fair participations.
Detailed breakdown of destructive testing standards, shear test rigs, and microstructure SEM inspection for laser joints on dry cutting circular saw discs.
Read Article →Showcasing our ultra-thin 1.0mm dry cutting ceramic discs and high-speed J-slot saw blades to global ceramic tool buyers at the Guangzhou Canton Fair Complex.
Read Article →Introducing JIAYAN's specialized sintered stone diamond cutting disc series to European slab fabricators and international OEM distributors.
Read Article →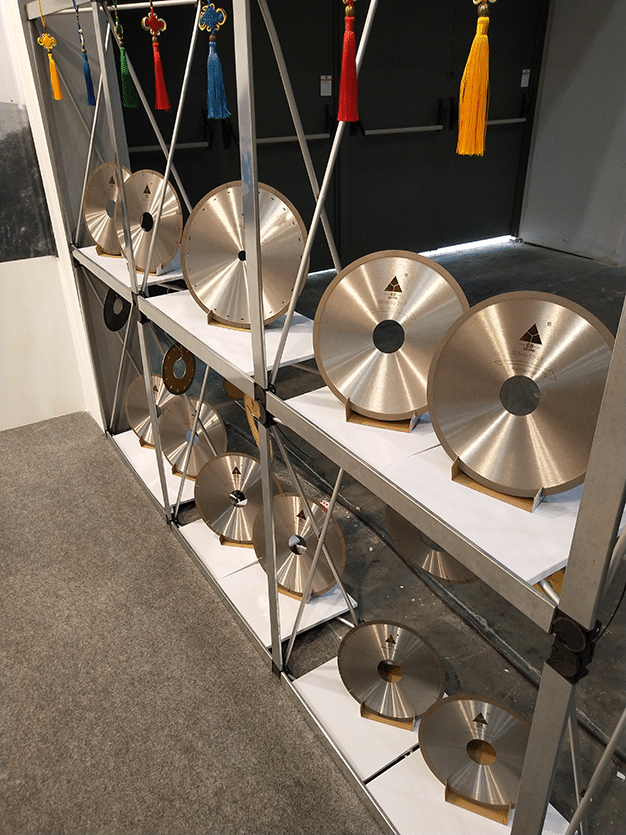
Ensuring global market access through rigorous international safety standard adherence and dust mitigation integration.
When exporting superhard tools to Europe, North America, and Australia, compliance with international safety norms is paramount. Industrial dry cutting tools operate at high angular velocity without water suppression, making structural blade integrity critical to operator safety.
All JIAYAN dry cutting saw blades are designed, tested, and certified in accordance with EN 13236 standard guidelines. Key compliance measures include:
Dry cutting of stone and concrete generates microscopic silica dust particles. Modern job sites demand saw blades compatible with dry vacuum shrouds and high-efficiency dust collection systems. JIAYAN saw discs feature aerodynamic slot designs that direct dust streams efficiently into vacuum shroud inlets, helping contractors meet strict OSHA silica safety regulations.
To support global distribution, our ODM team provides custom arbor sizing and precision reducers. Options include 22.23mm (7/8") for standard angle grinders, 25.4mm (1") for masonry saws, and 50mm/60mm heavy industrial bores with drive pin holes.
In-depth answers to common engineering, matrix formulation, and private-label ordering questions.
Dry cutting saw discs are specifically engineered with matrix metal bonds and laser-welded joints capable of withstanding extreme continuous heat (up to 800°C) without liquid cooling. Standard wet blades rely on water to flush slurry and cool the solder joint; using a wet blade dry will cause high-frequency solder joints to melt, leading to dangerous segment loss and core warping.
We utilize fully automated high-power fiber laser welding systems to fuse the sintered diamond segment directly to the 75Cr1 alloy steel body. This creates a deep metallurgical weld seam with shear strength exceeding 600 MPa. In addition, our titanium-coated synthetic diamond crystals prevent diamond pull-out by forming a tough chemical bond with the surrounding metal powder matrix.
For dense sintered stone (such as Dekton or Neolith), continuous turbo rim or J-slot designs with ultra-thin kerfs (1.0mm–1.4mm) are ideal. The J-slot relief cut allows core expansion and relieves lateral tension, while the micro-segmented turbo mesh rim provides smooth, chip-free top and bottom edge cuts.
Titanium coating acts as a thermal barrier that prevents oxidation and graphitization of diamond crystals under high temperatures. It also prevents chemical reactions between liquid metal powders and diamond carbon during sintering, significantly improving diamond holding force inside the metal matrix.
The inverse hardness rule applies: For hard, dense quartz granite, a softer metal matrix (rich in bronze and cobalt) is required so the matrix wears away continuously to expose sharp new diamonds. For highly abrasive, softer limestone or sandstone, a hard metal matrix (rich in iron, tungsten carbide, and nickel) is required to resist abrasive erosion and prevent premature diamond release.
Every industrial blade undergo strict dynamic balancing checks. Radial runout is maintained under ±0.03mm and axial runout under ±0.04mm. This eliminates hand-tool vibration, extends angle grinder motor life, and yields perfectly straight, clean cut lines.
We provide comprehensive private label customization, including laser-etched brand logos, specialized core paint finishes (matte black, electric blue, titanium silver, custom Pantone colors), custom arbor bore sizes, customized blade slot shapes, and branded blister or retail packaging.
Operating below recommended linear speeds causes diamond grit to polish or "glaze" rather than fracture and cut. For 115mm–125mm angle grinder discs, recommended operating speeds range between 10,000 RPM and 12,000 RPM (approx. 60–80 m/s peripheral velocity). If glazing occurs, dress the blade by making several cuts into abrasive dressing stone or silica brick.
For standard catalog sizes, our MOQ starts as low as 100 to 300 units. For fully customized ODM projects requiring specialized segment mold tooling, custom powder metallurgical formulations, or custom laser slot patterns, our standard MOQ is typically 500 units per specification.
Every shipment is accompanied by ISO 9001 Quality Inspection Certificates, EN 13236 Safety Compliance Test Reports, Segment Shear Strength Test Logs, and Mill Test Certificates for the underlying alloy steel cores.
Select high-performance diamond saw blades engineered for specialized stone and ceramic cutting applications.
China's Leading ODM/OEM Manufacturer of Premium Diamond Saw Blades & Superhard Tools. Member of China Superhard Material Association.
 JIAYAN Superhard Tools









