High-performance diamond saw blades engineered with proprietary powder metallurgy for granite, sintered stone, ceramic, and marble processing.



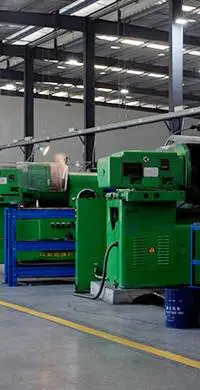
Founded in Wuhu, Anhui Province, China, JIAYAN Superhard Materials Co., Ltd. stands as a premier global OEM diamond saw blades supplier & exporter. As an active accredited member of the China Superhard Material Association, JIAYAN integrates advanced powder metallurgy, automated vacuum hot-pressing sintering, and state-of-the-art high-frequency laser welding technology to engineer industrial cutting tools for the modern stone and construction sectors.
Whether manufacturing ultra-thin continuous rim blades for delicate vitreous ceramic slabs or 350mm to 2000mm laser-welded diamond segments for abrasive volcanic granites, our technical workflow adheres strictly to ISO 9001:2015 quality assurance frameworks and EN13236 European safety parameters.

The diamond tool industry is undergoing a paradigm shift driven by engineered stone substrates, eco-conscious dry cutting regulations, and high-efficiency CNC bridge saw integration.
The rapid adoption of large-format sintered porcelain slabs (such as Dekton, Neolith, and Laminam) requires saw blades with extremely soft, self-sharpening bronze-cobalt matrices to eliminate micro-chipping and internal tension cracking along slab edges.
Environmental health and safety (EHS) laws in North America and Western Europe have made silent saw cores mandatory. By sandwiching copper or viscous rubber foil between steel core plates, cutting noise is suppressed by 10 to 15 dB(A).
With raw stone prices escalating, reducing kerf width from traditional 3.2mm down to 1.0mm–1.6mm yields substantial material savings per slab. High-tensile Japanese alloy steel cores ensure minimal blade deflection under high torque.
Transitioning from manual silver brazing to robotic fiber laser welding eliminates human error in segment attachment. The resulting metallurgical bond withstands thermal shocks up to 800°C without risk of segment loss during dry cutting.
To mitigate global supply chain volatilities and regulatory risks associated with pure cobalt powder, next-generation segment formulas utilize sub-micron iron-copper-nickel pre-alloyed powders that maintain high diamond retention at reduced cost.
Advanced 3D diamond array technology places synthetic diamond grit in precise grid positions throughout the segment volume, guaranteeing uniform wear rates, stable power consumption, and up to 30% longer tool life.
The cutting velocity and wear life of an OEM diamond saw blade are dictated by the tribological equilibrium between diamond grit degradation and matrix bond erosion.
JIAYAN utilizes monocrystalline and high-grade octahedral synthetic diamond grains synthesized under high-pressure, high-temperature (HPHT) conditions. Diamond grit parameters are strictly matched to the workpiece material:
The metal matrix must wear down at a rate synchronized with diamond crystal dulling. If the matrix is too hard, diamonds become glazed and burn the slab; if too soft, diamonds tear out prematurely:
| Substrate Material | Mohs Hardness | Recommended Bond Matrix | Optimum Diamond Mesh | Peripheral Speed (SFPM / m/s) |
|---|---|---|---|---|
| Class V Hard Granite (e.g., Red Multicolor) | 7.0 – 7.5 | Soft Bronze-Copper Matrix | 40/50 US Mesh | 25 – 30 m/s (Wet) |
| Class I-II Soft Granite / Basalt | 5.5 – 6.5 | Medium Iron-Cobalt Bond | 35/45 US Mesh | 30 – 35 m/s (Wet) |
| Calcareous Marble / Limestone | 3.0 – 4.0 | High Electroplated / Soft Sintered | 50/60 US Mesh | 40 – 50 m/s (Wet) |
| Sintered Stone / Dekton Slabs | 7.0 – 8.0 | Proprietary Ultra-Soft Pre-Alloy | 60/80 US Mesh | 18 – 22 m/s (Low RPM Wet) |
| Vitreous Porcelain & Ceramic Tile | 6.0 – 7.0 | Fine Bronze Continuous Rim | 80/100 US Mesh | 25 – 35 m/s (Dry/Wet) |
JIAYAN provides end-to-end manufacturing solutions for international brands, tool chain stores, and high-volume stone processors seeking tailored blade geometry and private label packaging.
We engineer specific segment geometries including Keyhole slots for rapid heat dissipation, J-Slots for chip prevention, W-Segment profiles for instant dressing, and Turbo Rim contours for smooth fast cutting.
High-precision fiber laser markers print your corporate logo, safety icon markings, barcodes, batch numbers, and rotational directional arrows directly onto steel cores prior to protective anti-rust coating.
From color retail blister packs and eco-friendly corrugated cartons to heavy-duty wooden crate export packaging with VCI anti-corrosion liners, we deliver retail-ready solutions tailored to your market.
To safeguard our global partners against raw material price spikes, JIAYAN offers scheduled blanket purchase orders, strategic steel core buffer stocking, and guaranteed 15-day manufacturing lead times.
Tailored operational configurations engineered for specialized processing equipment and severe jobsite conditions.
In large-scale stone processing facilities, multi-blade setups (utilizing up to 80 circular saw blades mounted on a single arbor) require absolute consistency in segment height, blade flatness, and side clearance.
Modern 5-axis CNC bridge saws require blades that perform complex 45-degree miter cuts, plunge cuts, and tight arc contours without causing edge blowout or machine spindle overload.
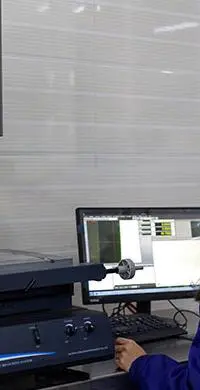
Safety and reliability are non-negotiable parameters in industrial superhard tooling. JIAYAN enforces rigorous multi-stage quality inspections on every production lot.
Sample blades from each production run undergo hydraulic torque shear testing according to EN13236 standards. Laser-welded segments must resist shear forces exceeding 450 MPa before lot approval.
Every steel core is dynamically balanced on micro-computerized testing rigs. Radial runout is strictly maintained below <0.03mm and axial runout below <0.02mm to eliminate saw chatter and uneven wear.
Our products comply fully with European Union Safety Standard EN13236, MPA Hannover certification guidelines, and REACH chemical safety standards regarding heavy-metal-free matrix formulations.
Our R&D division is continuously pioneering cutting-edge superhard material synthesis to solve tomorrow's industrial cutting challenges.
Titanium nano-coating of diamond synthetic crystals to prevent thermal oxidation during sintering, increasing diamond retention by 25%.
Embedding micro RFID vibration and thermal sensors into industrial saw cores for real-time monitoring of blade stress during heavy slab cutting.
Implementing automated AI vision-guided laser welding systems that dynamically inspect weld bead geometry at sub-micron levels.
Stay updated on JIAYAN's technical trade show appearances, product innovation releases, and industry research articles.
Technical evaluation of key inspection methodologies for laser-welded diamond saw blade joints — covering microscopic metallurgical joint examination and shear stress testing protocols.
JIAYAN showcased our latest high-speed continuous rim diamond circular blades at the Guangzhou Canton Fair Complex during the premiere Ceramic Industrial Technology Expo.
Presenting next-generation superhard tile cutting tools and ultra-thin segment discs to European stone fabricators and machine manufacturers in Rimini, Italy.
Detailed answers to technical B2B buyer inquiries regarding diamond blade selection, operating parameters, and OEM ordering.
Hot-Pressed Sintering fuses the diamond segment and steel core under simultaneous heat and pressure; it is optimal for continuous rim tile blades and small angle grinder discs. Laser Welding uses a high-energy laser beam to melt the steel base of the segment directly to the core plate, creating a metallurgical joint capable of withstanding extreme dry-cutting heat without segment loss. Brazing (Silver Soldering) uses a silver alloy filler metal; it is standard for wet-cutting multi-blades where water coolant prevents the solder from melting.
Remember the inverse rule: Hard Materials Require Soft Bonds; Soft Materials Require Hard Bonds. Hard quartz-rich granite rapidly dulls diamond grit, so a soft bronze/copper matrix is required to wear away easily and release fresh sharp diamonds. Soft calcareous marble is less abrasive to metal, so a harder matrix (or electroplated diamond layer) is used to prevent the core from wearing prematurely.
Segment detachment occurs due to: 1) Cutting dry with wet-only brazed blades (causing silver solder flow failure); 2) Excessive side-thrust or blade deflection; 3) Incorrect arbor fit causing severe radial impact loading. To prevent failure, ensure laser-welded blades are specified for dry cutting, verify spindle RPM matches blade limits, and check water coolant delivery on both sides of the blade core.
Glazing happens when the metal bond is too hard for the substrate, preventing the matrix from wearing down to expose fresh diamond edges. To dress (sharpen) a glazed blade, make several shallow cuts into an abrasive material like soft sandstone, green concrete, or an alumina dressing stick.
For standard stock sizes (e.g., 105mm, 115mm, 125mm, 230mm, 350mm), MOQ starts as low as 100 units. For custom segment formulas, non-standard arbor bores, or custom laser-etched branding packaging, MOQ is typically 300 to 500 units per specification.
For granite cutting with a 350mm (14") blade, target a peripheral speed of 25 to 30 m/s, corresponding to 1400 – 1750 RPM. For delicate porcelain/sintered stone slabs, lower the peripheral speed to 18 – 22 m/s (approx. 1000 – 1200 RPM) to prevent edge chipping.
Select from our comprehensive inventory of diamond saw blades and cutting discs engineered for international distribution.
Contact our technical engineering team today for factory-direct pricing, OEM sample evaluation, or customized blade development.