Explore our high-performance large stone cutter blades, hot-pressed diamond discs, and laser-welded cutting systems engineered for bridge saws, CNC workstations, and block cutters.








In the contemporary stone processing and dimensional quarrying sector, large stone cutter blades (ranging from 350mm to upwards of 3500mm in diameter) represent the core mechanical interface between high-torque industrial machinery and dense geological formations. As modern architectural demands shift toward hyper-dense materials such as quartzite, granites with high quartz content (Mohs hardness 6–7), and ultra-compact sintered stone slabs, the mechanical demands on circular saw blades have intensified exponentially.
A high-performance large stone cutter blade is an intricately balanced tribological system consisting of three fundamental components:
Dynamic stability during stone cutting dictates cut accuracy, edge chipping rates, and tool lifespan. As blade diameter increases, centrifugal forces and peripheral heat gradients induce thermal stress that can cause core warping if tensioning is compromised.
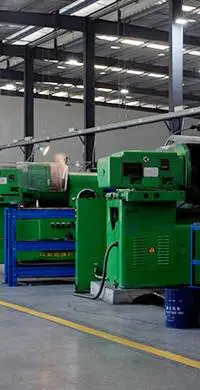
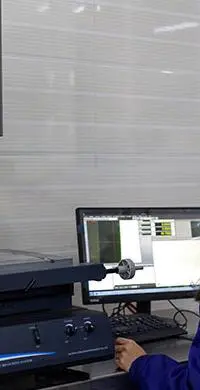
Headquartered in Wuhu, China, and operating as a core member of the China Superhard Material Association, JIAYAN integrates raw material synthesis, advanced powder sintering, automated laser welding, and strict quality control.
China produces over 90% of the world's industrial synthetic diamonds. Our location enables direct access to top-grade monocrystalline diamonds and ultrafine pre-alloyed powders, drastically reducing raw material costs and lead times.
Utilizing high-precision computer-controlled vacuum hot-pressing sintering machines, we ensure 100% density in segment matrixes, eliminating internal porosity and premature diamond fallout.
Fully automated German and Chinese laser welding stations fuse segments directly to the steel blank with deep metallurgical penetration, eliminating segment detachment during extreme high-speed or dry-cutting loads.
Complete OEM services: bespoke segment geometries (step, turbo, sandwich, fan-slot), custom laser marking, pantone color lacquering, silent resin slots, and custom arbor bore specifications for worldwide distributors.
The operational lifespan and cutting efficiency of a large diamond saw blade depend on the wear balance between the diamond grit and the sintered metal bond matrix.
Target Stone: Highly abrasive, soft stones (Sandstone, Soft Limestone, Abrasive Green Granites).
Formulated with high tungsten carbide and dense cobalt concentrations to resist excessive erosion, preventing premature diamond drop-out and ensuring extended square-meter cutting yield.
Target Stone: Class 2–4 Medium-Hard Granites, Basalts, Dense Dolomites, and Engineered Quartz.
The industry-standard universal formulation. Balances free-cutting speed with wear longevity across high-throughput industrial automated bridge saws and multi-blade block cutters.
Target Stone: Quartzite, Class 5 Hard Granite, Sintered Stone (Dekton), and Hard Porcelain.
Utilizes bronze, copper, and nickel binders that wear synchronously with the tough material, continuously exposing sharp, fresh diamond micro-edges to prevent blade glazing and high motor amperage draw.
| Blade Diameter Range | Standard Core Thickness | Segment Dimension (L×W×H) | Recommended Peripheral Speed ($v_c$) | Recommended Water Feed Rate | Primary Application |
|---|---|---|---|---|---|
| 300mm – 350mm (12"–14") | 2.2 mm – 2.6 mm | 40 × 3.0/3.2 × 10/12/15 mm | 28 – 35 m/s (1500–1900 RPM) | 15 – 25 L/min | CNC Bridge Saws, Slab Trimming, Sintered Stone |
| 400mm – 500mm (16"–20") | 2.8 mm – 3.5 mm | 40 × 3.6/4.0 × 12/15/20 mm | 26 – 32 m/s (1000–1500 RPM) | 25 – 40 L/min | Granite Countertop Fabrication, Kerbstone Cutting |
| 600mm – 900mm (24"–36") | 4.0 mm – 5.5 mm | 40/50 × 5.0/6.0 × 15/20 mm | 24 – 30 m/s (600–950 RPM) | 40 – 60 L/min | Monument Processing, Architectural Block Squaring |
| 1000mm – 2200mm (40"–88") | 6.0 mm – 8.0 mm | 24/30 × 7.0/8.5 × 15/20 mm | 20 – 28 m/s (250–500 RPM) | 80 – 150 L/min | Primary Quarry Block Extraction, Multi-Blade Gantry |
| 2500mm – 3500mm (100"–140") | 9.0 mm – 11.5 mm | 24 × 9.0/11.0 × 20/25 mm | 18 – 24 m/s (120–220 RPM) | 150 – 250 L/min | Mega-Block Squaring, Heavy Granite & Basalt Sawing |
As the international stone sector embraces automated 5-axis CNC machines, environmental noise regulations, and ultra-compact architectural surfaces, diamond blade engineering continues to advance.
Traditional solid steel cores create resonance frequencies exceeding 105 dB(A). Modern silent cores utilize a multi-layer composite construction—two hardened steel plates bonded around a microscopic copper or viscoelastic polymer acoustic dampening film. This reduces operating noise by up to 15 dB(A) and absorbs vibration to safeguard machine spindles.
Moving beyond randomized diamond grit dispersion, Arix (Arrayed Diamond) technology places synthetic diamond crystals in precise, equidistant geometric matrices throughout the bond volume. This guarantees a constant diamond exposure density per square millimeter, resulting in 50% faster cutting speeds and extended tool life.
Sintered stones are compacted at over 25,000 tons and fired at 1200°C+, creating exceptional surface hardness and high internal tension. Standard granite blades cause catastrophic edge breakout and micro-fractures. Specialized sintered stone blades feature ultra-fine diamond mesh (120/140 to 200/230) and specialized soft cobalt-free matrices to achieve clean, polished edges.
From quarry extraction in Brazil and India to high-speed architectural fabrication in Italy and North America, JIAYAN engineered blades deliver tailored cutting performance.
Operating Environment: High-torque gantry block cutters with multi-blade configurations (16 to 32 blades mounted simultaneously) slicing raw dimensional granite, basalt, or limestone blocks into standardized 20mm or 30mm slabs.
Operating Environment: Modern stone countertop fabrication facilities running automated bridge saws with automated mitering, plunging for sink cut-outs, and L-shaped corner cuts on quartz, granite, and porcelain.
Operating Environment: Fabrication of thick granite curbstones, structural bridge piers, retaining walls, and custom memorial monuments utilizing blades from 600mm to 1600mm.
Operating Environment: Precision continuous processing lines producing 6mm to 12mm large-format exterior cladding panels and interior flooring.
Procurement directors and factory operators must evaluate multiple mechanical and chemical parameters to optimize tool life and reduce cost per square meter.
Mesh Sizing: Coarser mesh (30/35, 35/40) delivers fast cutting in soft to medium granites; finer mesh (50/60, 70/80) produces clean edges on brittle quartzite and ceramic.
Concentration: 25%–35% for high-speed free cutting; 40%–60% for long-life industrial block squaring under high downfeed pressures.
Accurate center bore sizing (e.g., 50mm, 60mm, 80mm, 100mm, or custom 120mm) and drive pinholes (e.g., 6/M10 on 120mm PCD) prevent rotational slipping during rapid spindle acceleration and deceleration cycles.
True tooling economy is measured in cost per square meter ($/m²), factoring in cutting speed ($m^2/\text{hour}$), machine electrical load (kW), secondary chamfering reduction, and overall tool life ($m^2/\text{blade}$).
We provide full customization for global tool distributors, stone processing syndicates, and machinery manufacturers:
As an active member of the China Superhard Material Association with over a decade of direct export experience, JIAYAN serves industrial distributors, stone factories, and construction contractors across Europe, the Americas, the Middle East, and Southeast Asia.
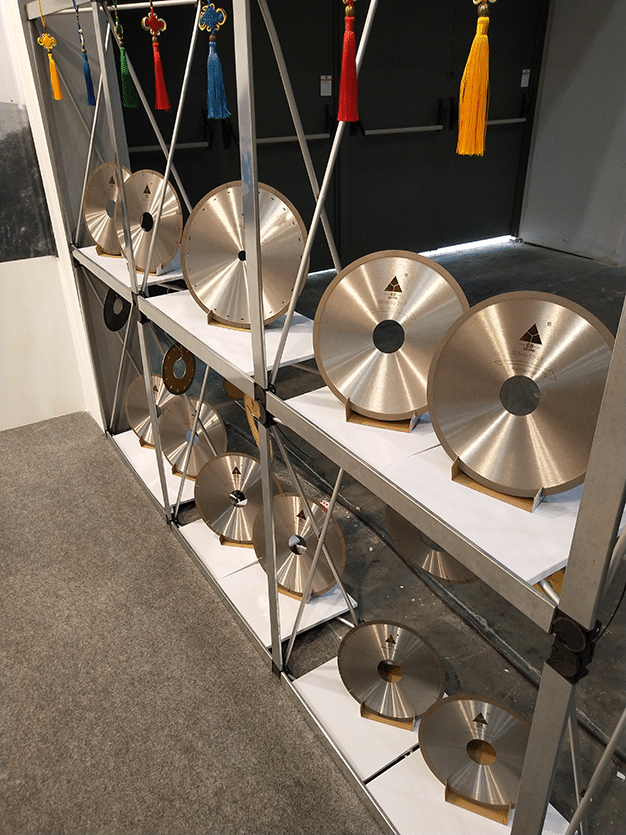
JIAYAN regularly presents its latest metallurgical innovations at premier global stone and ceramic technology expositions, including TECNARGILLA Rimini (Italy) and the China International Exhibition for Ceramic Technology & Equipment (Guangzhou Canton Fair Complex).
Our technical R&D team continuously publishes research on critical industry topics, including non-destructive laser weld strength verification, microstructural metallography of brazed diamond joints, and computerized dynamic balance tensioning.
Explore technical documentation, exhibition reports, and practical guides on diamond blade maintenance and weld inspection.
Comprehensive breakdown of appearance inspection, microstructure metallographic analysis, and destructive torque/shear testing to guarantee safety.
Presenting high-speed sintering continuous diamond cutting discs and ultra-thin ceramic cutting systems at the Canton Fair Complex.
Showcasing our specialized sintered stone blades and diamond discs to European ceramic and stone fabricators.
Technical answers to common questions about blade selection, matrix bonding, operating parameters, and maintenance.
High-frequency silver brazing uses a silver-copper solder alloy melting around 650°C–750°C, which requires constant water cooling during operation. Laser welding uses a high-density CNC laser beam to melt the steel core and segment transition layer together into a unified weld seam, withstanding temperatures over 900°C. This makes laser welding essential for heavy-duty dry cutting, safety-critical construction, and high-load automated bridge saws.
Glazing occurs when the metal bond matrix is too hard for the stone being processed, causing the diamond crystals to round off without the matrix eroding away to expose fresh diamond edges. To dress a glazed blade, run several cuts through an abrasive refractory brick, soft abrasive sandstone, or concrete block with reduced water flow to strip the glazed bond layer and re-expose sharp diamond tips.
Silent core blades use a sandwich construction of two outer hardened alloy steel sheets (typically 65Mn/75Cr1) with a micro-thin layer of acoustic copper foil or viscoelastic resin laminated in between. This composite core disrupts acoustic vibration wave propagation, attenuating high-frequency squeal by 10 to 15 dB(A) while dampening harmonic vibrations that can cause micro-chipping on delicate slabs.
Blade deviation typically results from four root causes: 1) Loss of dynamic core tension due to thermal overheating; 2) Uneven segment flank wear (tapered segments) creating side-tracking; 3) Excessive feed speed exceeding the blade's specific cutting energy capacity; or 4) Worn spindle bearings or misaligned blade flanges. Re-tensioning the steel blank and verifying flange runout (<0.02mm) resolves most tracking issues.
Sintered stone requires a specialized blade with: 1) A soft, cobalt-free bronze/copper matrix; 2) Ultra-fine diamond mesh (140/170 to 200/230 grit) to eliminate edge breakout; 3) Close-pitch narrow keyhole or continuous turbo rim geometry; and 4) Precise dynamic balance to avoid vibration. Operating parameters should maintain a peripheral speed of 28–32 m/s with a reduced entry and exit feed rate.
For standard sizes (350mm–600mm), our flexible OEM MOQ begins at 20–50 units per specification, with custom laser engraving and packaging. Production lead times for custom sintered formulas are typically 15 to 25 business days, supported by rapid air freight for pilot samples or sea container shipping for bulk wholesale distribution.
Direct sourcing from JIAYAN Superhard Tools: precision diamond saw blades, ultra-thin ceramic discs, and large granite circular cutters engineered for export.
Request an engineering consultation, customized segment bond trial, or wholesale container quote from China's trusted superhard diamond tool manufacturer.