Explore precision-engineered diamond saw blades and circular cutters manufactured to rigorous ISO 9001 and EN 13236 safety standards for high-speed industrial cutting operations.
A comprehensive examination of material evolution, high-rpm operational dynamics, and OEM manufacturing requirements in modern superhard cutting applications.
The global stone and surface fabrication market has undergone a dramatic transformation over the past decade. Traditional natural marble and soft limestones are increasingly augmented by ultradense engineered surfaces—most notably sintered stone slabs (such as Dekton, Neolith, and Lapitec), hard Class IV/V granites, and micro-grain porcelain tiles. These engineered materials feature Mohs hardness levels exceeding 7.5, extreme density, and high internal structural tension. Consequently, conventional circular saw blades experience rapid segment glazing, excessive thermal deviation, and edge chipping. Modern B2B buyers require specialized OEM round saw cutters engineered with tailored bond matrices and precise grain degradation profiles.
During continuous high-speed rotation (linear speeds between 25 m/s and 45 m/s), circular saw blades generate significant frictional heat at the contact zone between the diamond segment matrix and the substrate. If heat energy is inefficiently dissipated, thermal stress propagation causes core tension loss, resulting in radial blade wobble (flutter) and premature diamond grain pull-out. Leading OEM round saw cutter factories overcome these mechanical constraints through computer-modeled stress-relief slots (J-Slots, Key-Slots, laser expansion cuts) and silent core sandwich structures designed to absorb acoustic vibration while retaining longitudinal core rigidity.
For global procurement managers, stone processing conglomerates, and superhard tool distributors, sourcing from a dedicated OEM round saw cutter factory goes beyond simple unit purchasing. It requires rigorous structural validation: precise steel core dynamic balancing (ISO Class G2.5 compliance), controlled powder metallurgy sintering temperatures, high-strength laser-welded joint shear limits (>1800 MPa), and repeatable mass production consistency. JIAYAN Superhard Tools leverages advanced automated hot-pressing systems to supply global buyers with bespoke blade geometry and custom kerf configurations engineered for maximum productivity.
When cutting 12mm to 20mm sintered porcelain slabs, core deflection as minimal as 0.15mm can result in catastrophic slab cracking. Standard saw blades lack the dynamic tension gradient necessary to withstand lateral push forces during high feed rates. JIAYAN's proprietary OEM dynamic tensioning protocol ensures flat kerf alignment and zero edge chipping even under intensive continuous cutting production environments.
An in-depth technical analysis of superhard material synthesis, metal bond formulation chemistry, and segment structural geometries optimized for OEM production.
The core cutting efficiency of a round saw cutter relies on the micro-structural quality of synthetic monocrystalline diamond grains synthesized via High-Pressure High-Temperature (HPHT) methods. JIAYAN strictly specifies diamond grit size distributions ranging from mesh size 30/40 (for coarse block quarrying) to 60/80 (for ultra-smooth ceramic rim polishing).
Furthermore, the Thermal Impact Index (Ti) and Toughness-Impact Index (TTI) of the diamond crystal are carefully matched to the thermal profile of the target cutting medium. For highly abrasive granite applications, heavy-duty cubo-octahedral diamonds with high thermal stability (resisting graphitization up to 1100°C) are integrated into the matrix to prevent premature micro-fracturing under impact loads.
The metal matrix (segment bond) acts as a structural anchor that holds individual diamond crystals until they become dulled, releasing them at a controlled rate to expose fresh sharp diamond points underneath—a process known as self-sharpening wear equilibrium. JIAYAN utilizes complex multi-element alloy matrices including Cobalt (Co), Nickel (Ni), Copper (Cu), Iron (Fe), and Tungsten Carbide (WC).
In high-rpm dry or wet cutting environments, segment detachment poses severe structural and safety hazards. JIAYAN operates fully automated CO2 and Nd:YAG laser welding lines. Laser welding creates a direct metallurgical atomic bond between the steel core key-way and the segment's metal transition zone, delivering shear strength ratings exceeding 1800 MPa—far surpassing traditional silver-brazed joints (approx. 600–800 MPa). This ensures maximum operator safety under heavy feeding pressures.
Tool geometry dictates debris removal speed and coolant fluid dynamic distribution. Standard segmented profiles provide aggressive debris clearance; J-Slot geometries relieve rim stress while maintaining continuous edge stability; Continuous Turbo rims provide consistent shear pressure required for chip-free cuts on delicate ceramic glazes. JIAYAN's OEM facility engineers custom segment slots (wavy, mesh, staggered keyhole) based on specific customer operational machinery.
Industrial stone cutting factories face stringent workplace environmental acoustic regulations (e.g., EU Directive 2003/10/EC). Standard solid steel core blades radiate high-frequency resonance frequencies during high-speed engagement. JIAYAN's OEM Silent Core saw blades incorporate a micro-thin copper layer laminated between two hardened tool-steel plates. This sandwich structure dampens harmonic acoustic resonance, reducing operational decibel output by up to 15 dB(A).
Reference specification matrix for engineering teams, procurement directors, and plant managers configuring custom OEM round saw cutter orders.
| Blade Diameter (mm / Inch) | Bore Size Range (mm) | Standard Segment Dimensions (L x W x H) | Recommended RPM Range | Peripheral Speed (m/s) | Target Material Application |
|---|---|---|---|---|---|
| 115 mm / 4.5" | 20.0 / 22.23 | Continuous Turbo / 1.2 - 2.0 mm Thickness | 10,000 – 13,200 RPM | 60 – 80 m/s | Ceramic Tile, Porcelain Slabs, Thin Marble (Dry/Wet) |
| 230 mm / 9" | 22.23 / 25.4 / 30.0 | 40 x 2.6 x 10 / 12 mm | 5,500 – 6,600 RPM | 65 – 80 m/s | Hard Granite Cladding, Masonry, Quartzite (Wet/Dry) |
| 350 mm / 14" | 50.0 / 60.0 / 70.0 | 40 x 3.2 / 3.6 x 15 / 20 mm | 1,450 – 2,100 RPM | 30 – 40 m/s | Granite Slabs, Sintered Stone Slabs (Bridge Saw - Wet) |
| 400 mm / 16" | 50.0 / 60.0 | 40 x 3.6 / 4.0 x 15 / 20 mm | 1,250 – 1,800 RPM | 30 – 40 m/s | Heavy Granite Slabs, Hard Quartzite, Concrete Blocks |
| 500 mm / 20" | 50.0 / 60.0 | 40 x 4.2 x 15 / 20 mm | 1,000 – 1,450 RPM | 28 – 38 m/s | Architectural Stone Dimensioning, Medium Granite Blocks |
| 800 mm – 1200 mm | 60.0 / 80.0 / 100.0 | 24 x 6.0 - 8.0 x 15 / 30 mm | 500 – 900 RPM | 25 – 35 m/s | Primary Block Quarrying, Heavy Masonry Trimming (Wet) |
How JIAYAN partners with international brands, tool importers, and industrial stone processing plants to deliver custom-branded superhard cutting solutions.
Every OEM partnership begins with detailed engineering evaluation. Our technical team analyzes your target material matrix (e.g., hard quartzite, soft marble, ultra-compact ceramics), machine parameters (bridge saw kW rating, spindle speed, water cooling pressure), and feed rates (m/min). This data informs the optimal bond hardiness and diamond concentration level.
High-grade 75Cr1 steel plates undergo automatic computer tensioning and laser-assisted dynamic balancing. Core tensioning prevents axial deflection under operational heat expansion. Radius runout is verified under tight sub-0.02mm tolerances, ensuring smooth, vibration-free blade rotation that protects machine spindles from excessive wear.
We provide full white-label and OEM private branding services. This includes high-resolution fiber-laser logo etching directly on the steel core, customized surface color coatings (powder coating, electroplating, epoxy paint), branded plastic display sleeves, color box design, and international barcoding/QR tracking integration.
Real-world performance evaluations of JIAYAN OEM round saw cutters across key global markets and specialized material fabrication environments.
Operational Challenge: High-end European kitchen countertop fabricators processing large-format porcelain slabs (6mm to 20mm Dekton/Neolith) encountered high micro-chipping rates and edge blowout when using standard granite blades on automated 5-axis CNC bridge saws.
OEM Solution: JIAYAN developed a custom 350mm continuous-rim J-Slot saw blade featuring a fine-mesh 50/70 diamond grit matrix bound in a soft bronze-nickel matrix. The J-Slot geometry dissipates lateral stress, allowing clean 45-degree miter cuts at feed rates up to 2.5 meters/minute with zero edge chipping.
Operational Challenge: Dimensional stone quarries processing abrasive Class V granites (e.g., Barre Gray, Dakota Mahogany) required heavy-duty 800mm to 1200mm circular saw blades capable of enduring continuous multi-shift block trimming without segment loss or core deformation.
OEM Solution: JIAYAN engineered laser-welded sandwich segments utilizing coarse 30/40 synthetic diamonds with a heavy cobalt-tungsten bond matrix. Combined with a heavy-duty 75Cr1 steel plate core, the blades achieved a 35% increase in total square-meter cut life while maintaining clean cut lines under high feed pressures.
Operational Challenge: Automated ceramic tile manufacturing facilities operating 24/7 continuous sizing line cutters needed ultra-thin 115mm to 230mm discs that minimize kerf material loss while maintaining high linear cutting speeds.
OEM Solution: JIAYAN supplied ultra-thin 1.0mm/1.2mm hot-pressed continuous turbo cutting discs with micro-grain diamond distribution. The reduced kerf thickness decreased power consumption by 18% and extended continuous operation intervals, reducing overall factory tooling expenditure.
Operational Challenge: Commercial construction projects cutting dense quartzite and thick Saudi limestone cladding panels faced strict municipal noise pollution codes alongside high ambient operating temperatures (over 45°C).
OEM Solution: JIAYAN delivered 400mm Silent-Core sandwich round saw blades configured with high thermal-dissipation keyhole water channels. The blades operated within strict decibel thresholds while sustaining high cutting performance under extreme heat conditions.
JIAYAN Superhard Tools enforces a zero-defect quality management framework compliant with global safety standards and environmental regulations.
All OEM round saw cutters manufactured in our factory strictly conform to European Standard EN 13236 ("Safety requirements for superhard abrasive products"). Every production batch undergoes destructive segment shear testing, high-speed burst testing (executing rotations up to 1.5 times maximum operational speed), and axial runout verification before international dispatch.
Our manufacturing facility operates under certified ISO 9001:2015 quality protocols. Standardized production control tracks raw metal powder purity, synthetic diamond micro-structural integrity, hot-pressing temperature curves (controlled to within ±2°C), and automated laser welding parameters. Full lot traceability ensures consistent performance across repeat orders.
Environmental stewardship and worker safety are core priorities. JIAYAN's metallurgical R&D lab has replaced toxic heavy metal additives with environmentally responsible alloy compositions. Our segment matrices are fully compliant with EU REACH and RoHS regulations, excluding cadmium and lead hazardous substances.
Leading the superhard tool industry through advanced sensor integration, nano-engineered diamond coatings, and automated eco-friendly manufacturing technologies.
Future round saw cutters will feature embedded micro-thin thermal and strain sensors within the core steel plate. These sensors communicate via telemetry with smart CNC bridge saws, providing real-time feedback on kerf thermal build-up and dynamic deflection. This allows automated feed rate adjustments that prevent blade jamming and extend tool life.
Next-generation diamond matrices incorporate Ti-coated (Titanium-coated) and CVD nano-layered diamond grains. Chemical bonding between the metal matrix and the titanium coating increases diamond retention strength by over 40%, virtually eliminating premature grain pull-out and maximizing structural grit utilization during hard stone cutting.
To reduce factory carbon footprints, JIAYAN is pioneering ultra-low energy pulse electric current sintering (PECS/SPS). This technology densifies segment metal powder matrices in seconds rather than minutes, reducing manufacturing energy consumption by up to 50% while producing denser, higher-performance tool segments.
Detailed technical answers to common queries raised by tool distributors, stone processing engineers, and procurement managers.
Founded in Wuhu, China, JIAYAN Superhard is an active member of the China Superhard Material Association, bringing over a decade of international OEM export excellence.

Operating automated cold-pressing, vacuum hot-sintering, and high-precision laser-welding lines, JIAYAN delivers superhard cutting tools serving over 50 countries across Europe, the Americas, the Middle East, and Southeast Asia.
Request Technical Catalog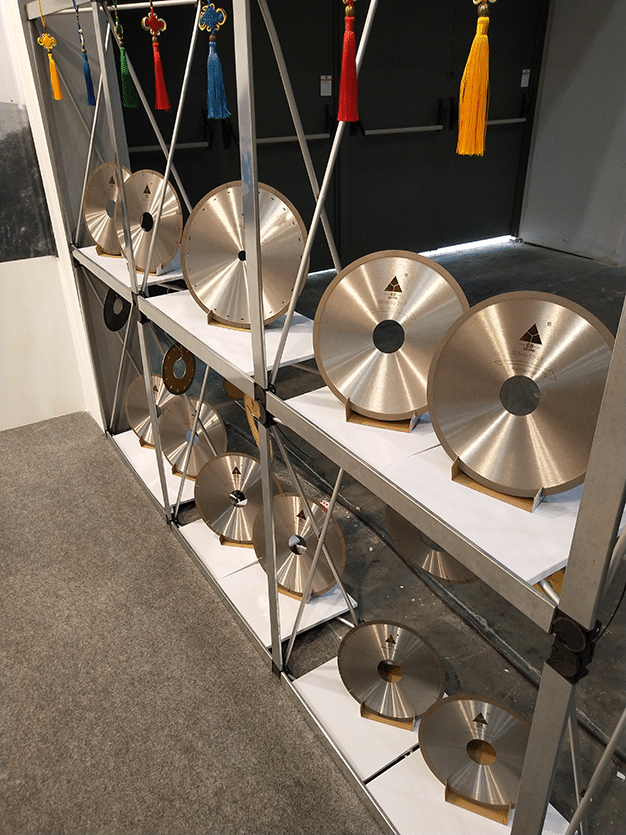
Regularly exhibiting at international industry events including TECNARGILLA Rimini (Italy) and the China International Ceramic Technology Exhibition (Guangzhou), JIAYAN continuously advances cutting tool technology alongside global partners.
Explore Industry Insights
Automated vacuum hot pressing ensuring matrix density and uniform diamond distribution.

Comprehensive shear, tension, and runout inspection protocols for guaranteed operator safety.
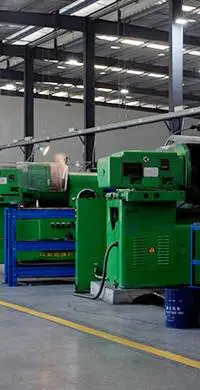
Large-scale manufacturing capacity delivering short lead times for high-volume orders.
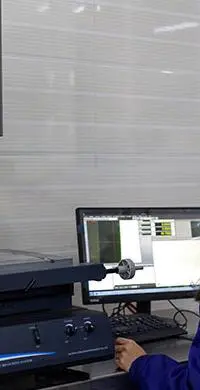
Complete custom private-label branding, custom packaging, and flexible logistics support.
Review our core line of high-performance diamond saw blades. Click any product to explore detailed specifications or submit an OEM customized production request.










