Precision-calibrated diamond circular blades and cutting discs engineered for heavy-duty granite cutting and delicate architectural ceramics across Vitebsk enterprises.
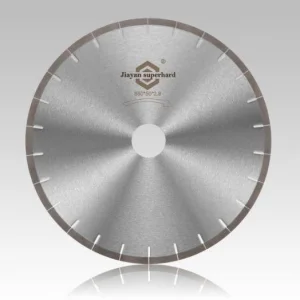
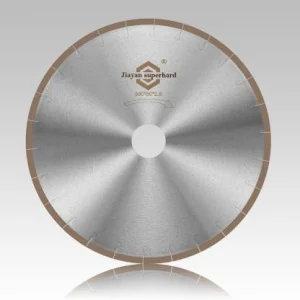
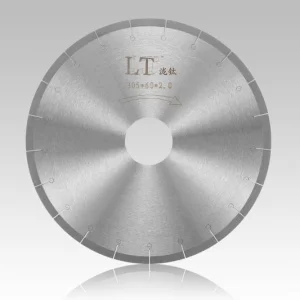
Navigating harsh continental climates, massive logistical hubs, and specialized structural masonry requirements across northern Belarus.
The Vitebsk Region serves as an indispensable manufacturing and logistic corridor within the Eurasian trade routes. Current investments into commercial infrastructure, transport facilities, and civic historic restorations demand large-format granite slabs, engineered quartz facades, and heavy quartzite curbstones. Such rigorous schedules require industrial saw blades that minimize machine downtime while maintaining clean, chip-free kerfs.
Vitebsk's continental climate experiences deep winter temperature dips. Unheated or semi-heated secondary processing workshops subject wet-cutting blades to extreme thermal swings. Our custom steel cores utilize high-tensile 75Cr1 and 65Mn spring alloys heat-treated to resist micro-fissuring, distortion, and loss of tension when cutting dense granites during sub-zero operational cycles.
Faced with high logistics costs on imported raw stone blocks, stone cutters in Vitebsk cannot afford segment detachment, blade deflection, or wide tolerances. By utilizing sandwich-type cobalt-bronze bonded matrices with coated synthetic diamond crystals, our tools ensure a thinner kerf, lower energy draw per square meter cut, and up to 28% longer operating life.
Precision-matched bonding systems developed by China Superhard Material Association metallurgical specialists for bridge saws, stationary gantries, and manual angle grinders.
| Blade Series Code | Diameter Range (mm) | Matrix Alloy Formulation | Target Material in Vitebsk Region | Optimum Peripheral Speed (m/s) |
|---|---|---|---|---|
| JY-GR-VTB (Granite Pro) | 300 – 600 mm | Cobalt-Tungsten-Copper Hot-Pressed Sintered | Gabbro, Red Granite, Basalt, Hard Diabase | 28 – 35 m/s (Wet) |
| JY-ST-CER (Sintered Spec) | 250 – 400 mm | Fine-Grained Bronze-Nickel Soft-Medium Bond | Large Porcelains, Dekton, Lapitec, Neolith | 25 – 32 m/s (Wet) |
| JY-JS-TURBO (Multi-Slot) | 115 – 230 mm | J-Slot Segmented Reinforced Steel Core | Ceramic Tiles, Marble, Vitrified Brick, Facades | 45 – 60 m/s (Dry/Wet) |
| JY-CON-HVY (Civil Infra) | 350 – 800 mm | Laser-Welded Carbide Reinforcement | Reinforced Concrete, Curbstones, Dense Asphalt | 35 – 45 m/s (Wet/Dry) |
Addressing every milestone from diamond crystal grit optimization to customs clearance in the Vitebsk Special Economic Zone (FEZ Vitebsk).
Stone parameters vary significantly across regional deposits. We adjust diamond synthetic crystal grade (e.g., high-purity Ti-doped crystals), diamond mesh size (30/35 to 70/80 mesh), and segment bonding densities specifically calibrated for hard crystalline quartzites or delicate glazed ceramics. Custom water slot geometry (U-slot, Keyhole, Narrow-slot, J-slot) maximizes coolant penetration and swarf ejection.
As a reputable exporter, JIAYAN supports Vitebsk clients with transparent multimodal transport routes (China-Europe Rail Express direct hub delivery to Vitebsk/Minsk terminals), full compliance documentation, Eurasian Economic Union conformity declarations, Certificate of Origin (Form A/General), and specialized anti-corrosion VCI packaging protecting against moisture during transit.
How progressive R&D is shaping diamond blade efficiency, automated laser manufacturing, and eco-friendly silent blade cores.
Transitioning from random crystal dispersion to three-dimensional matrix alignment ensures every synthetic diamond particle contributes equally to the micro-chipping process. This yields an identical feed rate throughout the segment's full lifespan, increases tool endurance by up to 40%, and reduces cutting resistance by 20%.
Vitebsk municipal indoor manufacturing plants increasingly enforce strict acoustic emissions legislation. Our sandwich-structured steel blanks—containing micro-thin copper laminates between hardened steel layers—dampen harmonic resonance, reducing operating noise by 10 to 15 dB while eliminating blade flutter.
For sintered stone slabs containing high resin and porcelain glass binders, conventional sintered segments may glaze over. Our vacuum-brazed hybrid peripheral discs expose razor-sharp monocrystalline diamonds directly, ensuring immediate bite without dressing and zero edge breakout on 45-degree miter cuts.
Comprehensive technical guidance on blade selection, RPM calibration, coolant flow, and bulk order logistics.
Hardness classifications determine matrix bonding: dense, quartz-rich granite and diabase stone require a softer cobalt-bronze matrix bond. A softer bond wears away at a rate that continuously exposes fresh, razor-sharp synthetic diamond edges, preventing segment glazing and tool overheating. For softer marbles or abrasive sandstone, a harder cobalt-tungsten matrix is recommended to maintain shape and segment geometry.
Yes. We produce standard 50mm and 60mm center bores with 10mm/12mm drive pin holes matching prominent machinery (such as Breton, Donatoni, Pedrini, GMM, and modern Chinese-manufactured gantries). Custom reduction rings (60mm to 50mm, 32mm, 25.4mm) with anti-slip drive patterns are also provided per drawing specifications.
For standard 350mm (14") blades cutting medium-to-hard granite, an operating spindle speed of 1800 to 2200 RPM is optimal (linear velocity of roughly 30–35 m/s). An uninterrupted water flow of at least 15 to 25 liters per minute must be focused directly into the cutting kerf to flush pulverized rock sludge and stabilize core temperature.
For standard catalog items, our flexible MOQ is 5 to 10 units per specification. Custom laser-engraved OEM branding or proprietary segment geometries require an MOQ of 50 units. Typical production turnaround is 15–20 days, followed by direct rail transport delivering to regional terminals within 18 to 25 days.
Explore our core product lineup trusted across European manufacturing facilities, stone masonry yards, and tile distribution hubs.
Empower your Vitebsk stone fabrication facility with precision-graded diamond cutting blades engineered for maximum square-meter yield, clean edges, and reduced maintenance costs.